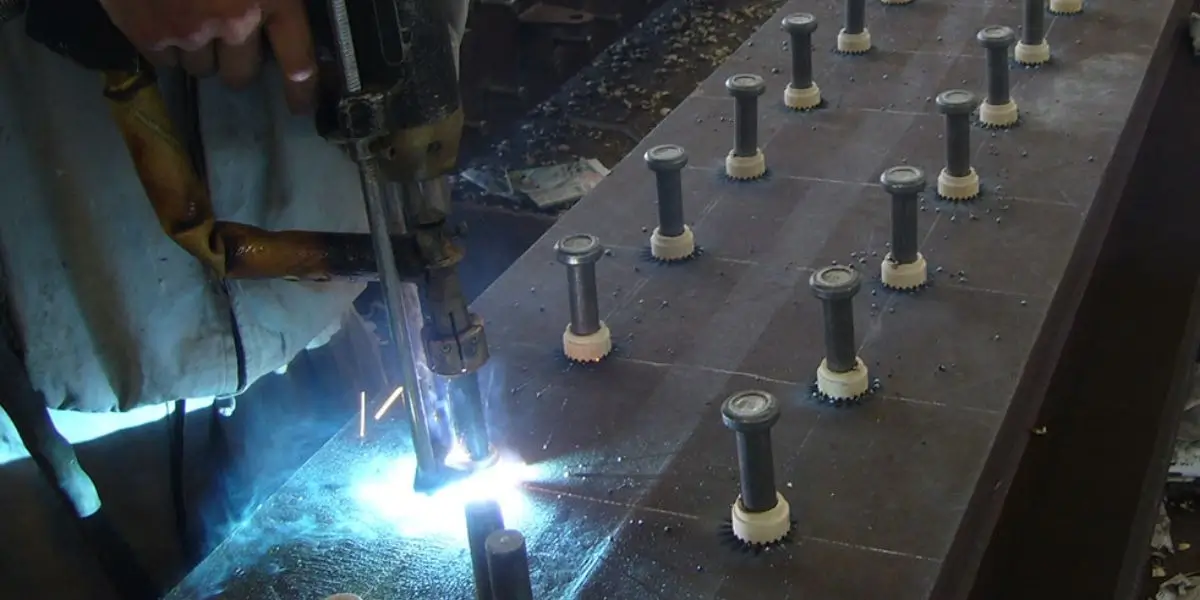
What is stud welding? It is a way to join a metal stud, pin or similar fastener to a metal workpiece by melting the stud end and a small area of the base metal, then pressing them together. The operator works from one side. For heavy steel construction, the usual concern is whether the specified stud and weld can transfer the design load, not how quickly the gun fires.
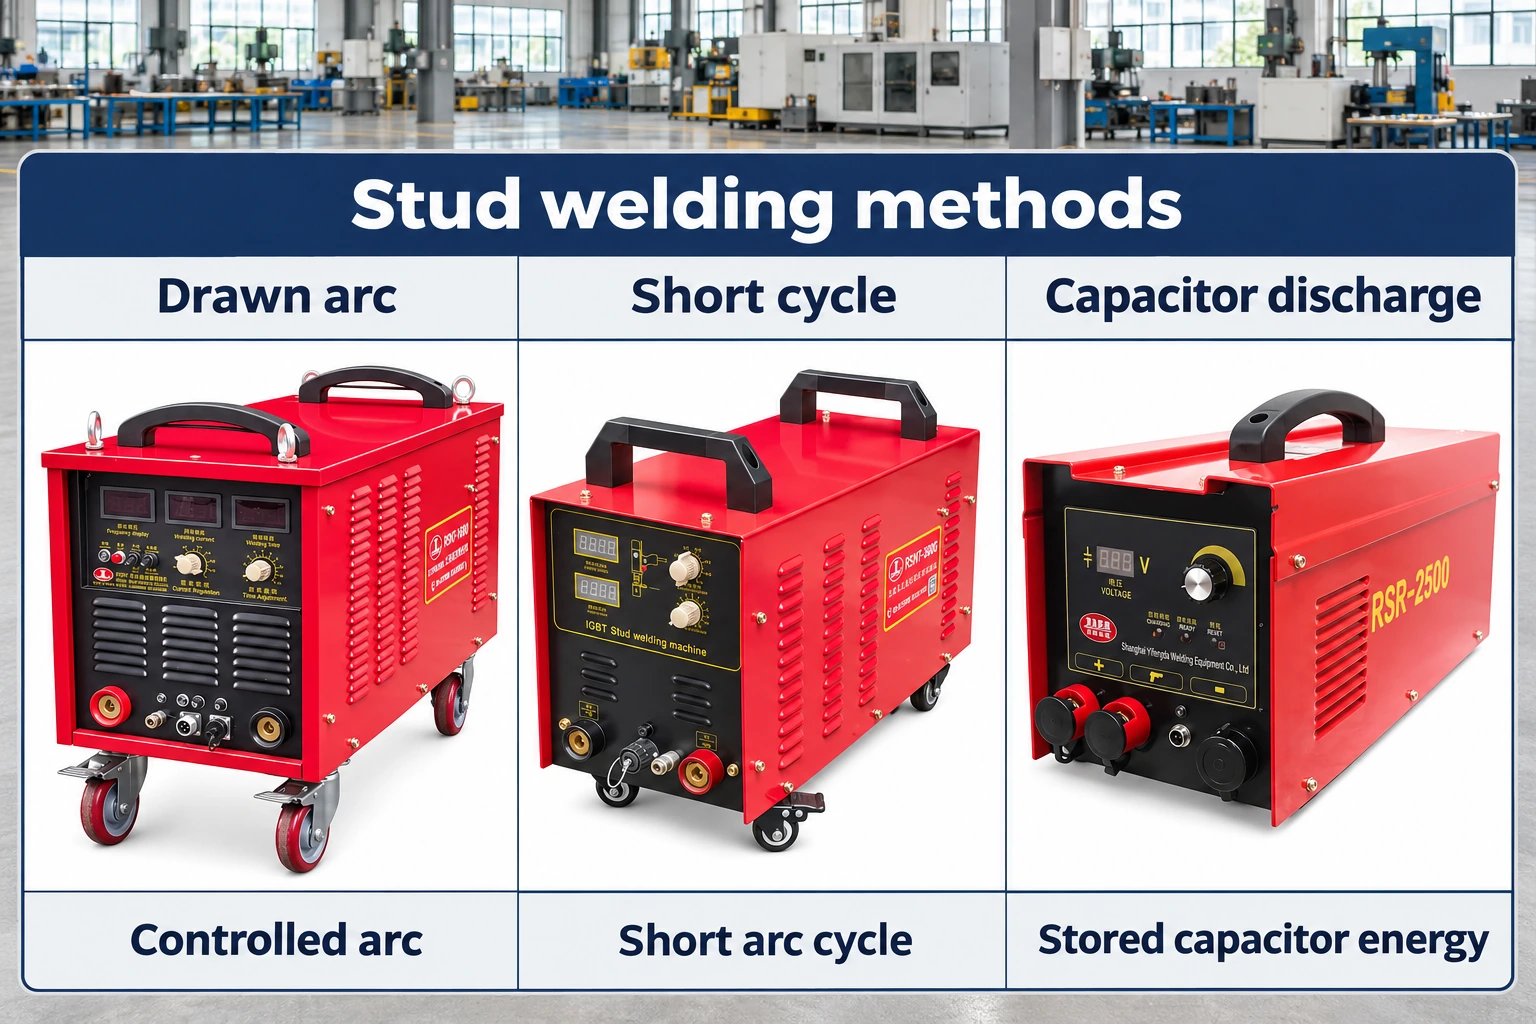
Stud welding includes several processes. This guide concentrates on drawn arc welding for structural studs, while also explaining where short cycle and capacitor discharge (CD) welding fit. The equipment, surface and inspection requirements change with the job.
For a better understanding of technical terms used in stud welding, explore our complete stud welding terminology guide.
How Drawn Arc Stud Welding Works
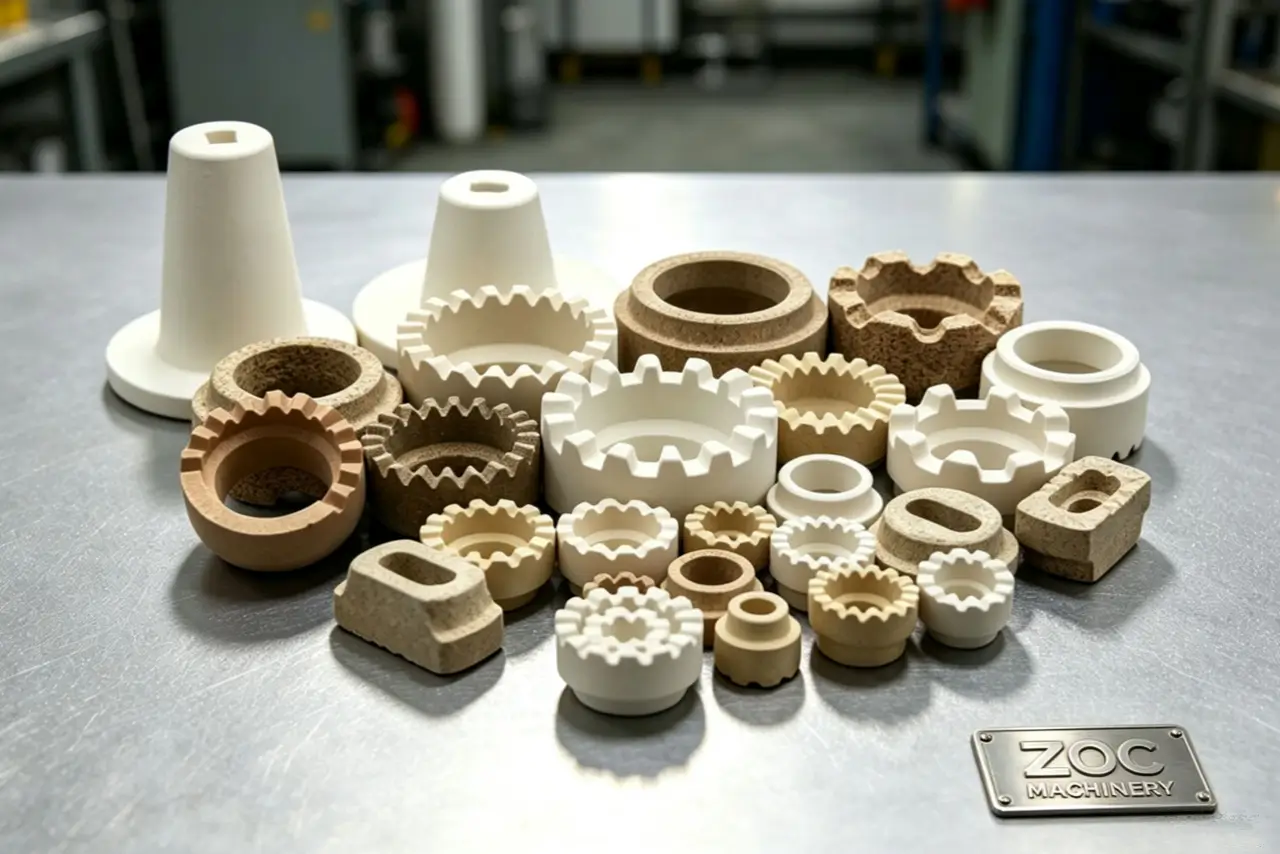
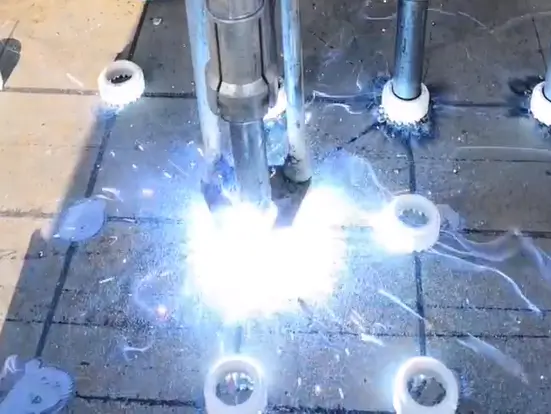
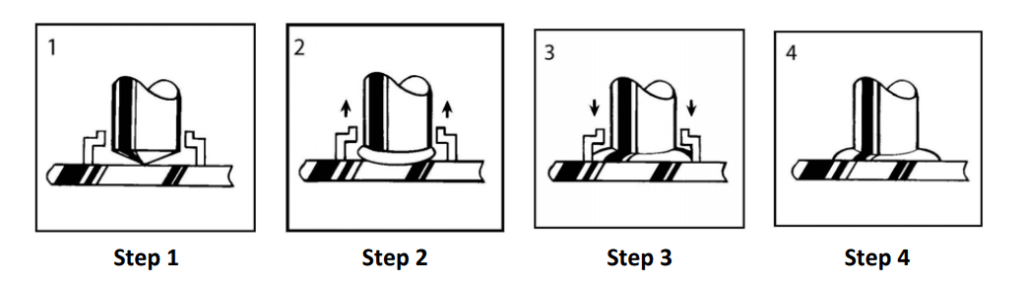
In Drawn Arc Stud Welding, a gun holds the stud against the steel, lifts it to establish an arc, then plunges it into the molten pool. Current and weld time control the heat; lift, plunge and contact with the base metal affect the result. A matching ceramic ferrule is often used to contain the molten metal and form the collar.
- Position: load the specified stud and ferrule, prepare the weld area and set the gun square to the work.
- Lift and arc: the gun lifts the stud and the arc melts the stud end and the workpiece.
- Plunge: the gun returns the stud into the molten pool at the programmed point.
- Cool and inspect: remove the ferrule after cooling and apply the required checks.
The cycle is automated, but a good weld is not automatic. Loose return leads, a dirty flange, the wrong ferrule or a gun that cannot move freely can spoil a setting that worked in the shop.
When Stud Welding Helps Compared with Drilling or Bolting
A welded stud can avoid a through-hole and separate nut where the design permits a permanent attachment. One-sided access is useful on a closed section or an assembled component. On repeated layouts, the short weld cycle can reduce handling and assembly steps.
Those benefits have limits. The completed rate includes positioning, surface preparation, ferrule handling and inspection. A weld does not automatically exceed the strength of the stud or leave a watertight assembly; both depend on the part, weld procedure and surrounding design. For a removable joint, a bolt may still be the better choice.
Main Stud Welding Processes
Process names describe different heat sources and cycles. They are not interchangeable labels for one machine. Check the stud and base-metal thickness against the equipment data and the approved procedure before choosing.
| Process | Common fit | What to verify |
|---|---|---|
| Drawn arc | Structural studs and heavier sections | Stud size, ferrule or shielding, power and procedure |
| Short cycle | Some smaller studs and thinner sections | Material, shielding and required joint performance |
| Capacitor discharge (CD) | Small studs on sheet metal | Stud tip, sheet thickness and reverse-face finish |
There is no single diameter or plate-thickness boundary that makes a process code compliant. A structural drawing and its governing specification decide what connection is required; trial welds and qualification show whether the proposed setup can make it.
Where Heavy-Duty Stud Welding Is Used
Steel buildings and bridges
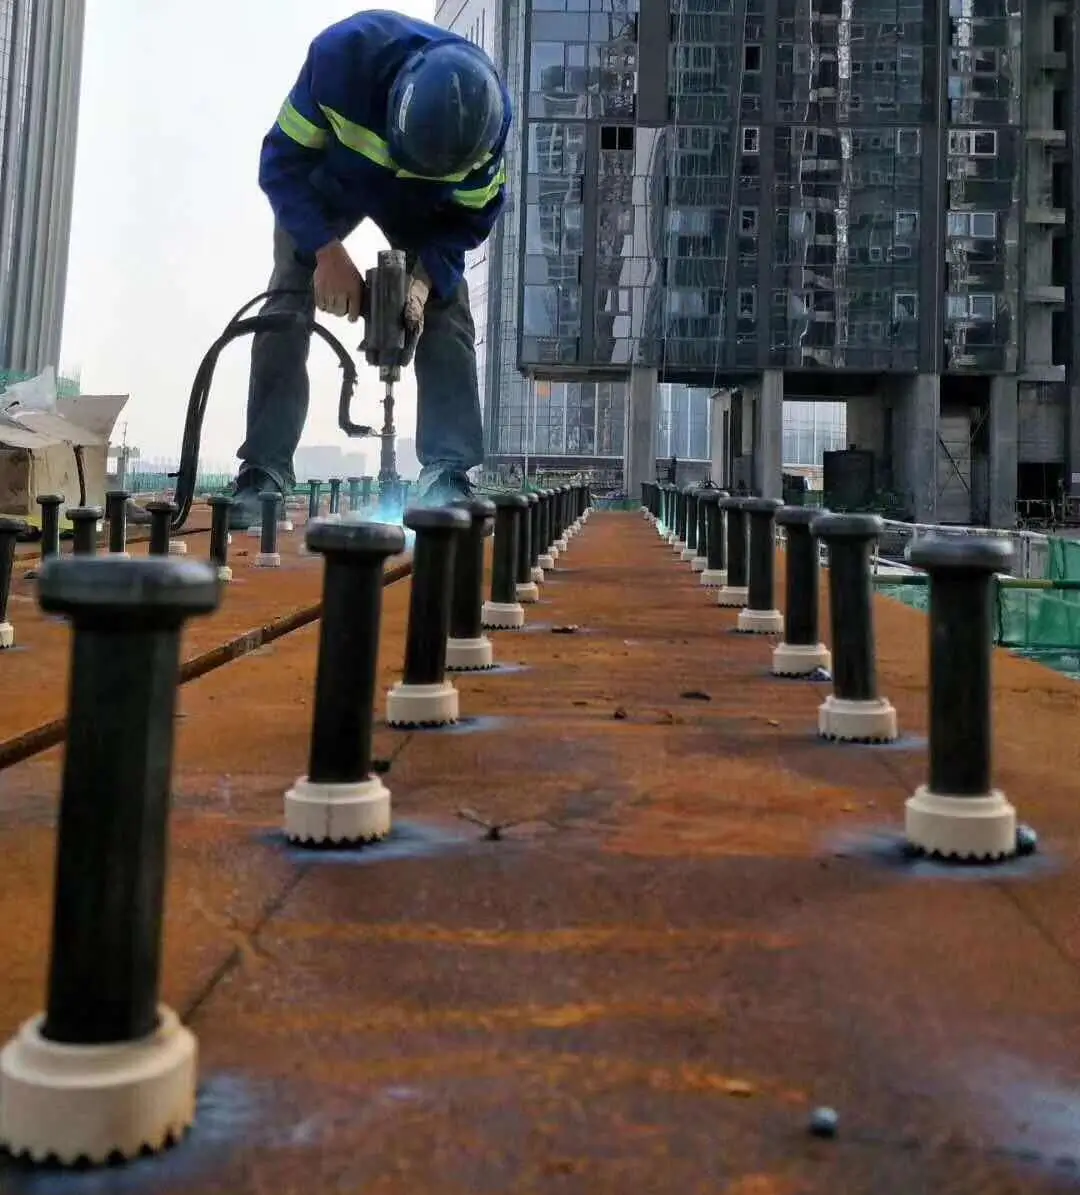
Headed shear studs are welded to steel beams and embedded in concrete so the beam and slab can act together. The designer sets stud size, spacing and location. Our shear stud explanation covers the structural role, and the shear stud range shows the supplied parts.
Some drawn arc stud designs use an aluminum flux ball at the weld tip to help initiate and stabilize the arc. That component is fitted during stud manufacture; the flux-fixing equipment does not replace the site welding procedure. Through-deck welding across galvanized decking is possible when the project detail and welding procedure allow it.
Shipbuilding and marine fabrication
Studs can hold cable trays, insulation or other attachments where a designer wants to avoid drilling through a plate. The weld does not make a ship hull automatically watertight or corrosion resistant. The hull detail, coating repair and inspection requirements still control acceptance.
Power and high-temperature equipment
Pins and anchors can secure refractory or insulation linings to steel casings. These parts differ from structural shear studs in geometry and service conditions. Specify the fastener material and temperature requirements before choosing a stud or welding system.
Equipment for Structural Stud Welding
Treat the power source, gun, leads, stud and ferrule as a matched system. Compare rated current and duty cycle with the specified stud sizes and planned production rate. Site input power, cable length and return-lead placement matter as much as the headline machine output.
Power source and controls
The ZOC RSN7 Inverter Series is one equipment option for drawn arc work. Ask which stud diameters it supports, its published duty cycle and the available current and time settings. Verify the proposed configuration with test welds on the project material instead of assuming a machine series guarantees a compliant weld.
Gun, cables and work connection
Heavy-duty guns hold the stud, control lift and plunge, and need the correct chuck and foot assembly. Inspect moving parts and cable connections before production. An uneven return path can affect the arc and collar, particularly near a plate edge.
Studs and ferrules
Order studs by drawing: diameter, length, head or thread, material and weld-end design. The ceramic ferrule range includes different shapes; use the one specified for the stud and welding position. ISO 13918 covers studs and ferrules as related components.
How to Check Weld Quality
For structural steel, use the inspection and test plan in the governing project documents. ISO 14555 addresses arc stud welding procedure and production testing; AWS D1.1 has stud welding requirements when the contract calls for it. Neither makes a single bend angle or test frequency universal for every job.
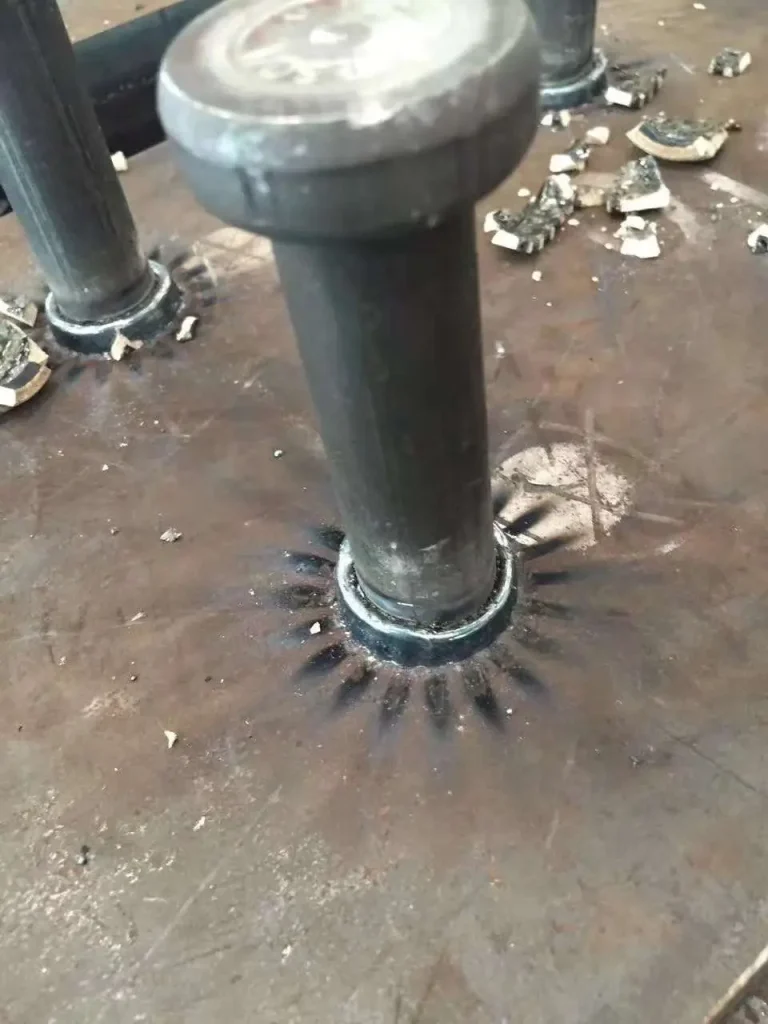
Inspect the cooled weld for obvious collar, crack and alignment problems, then perform the specified mechanical tests. A uniform collar is useful evidence, but it does not by itself prove fusion or strength. The stud welding quality guide separates visual checks from test results, and the troubleshooting guide helps diagnose a failed setup.
What to Ask a Supplier
Provide the stud drawing, base-metal grade and thickness, deck or coating detail, expected weld rate, site power and governing code. ZOC Machinery can then match a machine, gun, studs and ferrules to the job and identify what is included in the quotation.
Ask for a trial on representative steel and keep its settings, inspection and test results. Product documents, machine specifications and installed-weld records answer different questions; collect all three before accepting a structural stud welding system.
Send the drawing and production requirements with your inquiry. Request a Technical Consultation & Free Quote Today!
FAQs About Industrial Stud Welding
Are ceramic ferrules always required?
They are common in ferrule-shielded drawn arc welding, especially for structural studs. Other approved procedures may use different shielding. Follow the specified stud, ferrule and procedure.
Can studs be welded through galvanized decking?
Through-deck welding is used in some composite floors. Confirm the deck profile, unpainted beam flange, equipment and approved trial welds before production.
How do drawn arc and CD differ?
Drawn Arc stud welding lifts the stud and sustains an arc before plunge, while Capacitor Discharge (CD) welding releases stored capacitor energy in a brief pulse. CD is often chosen for small studs on sheet, and drawn arc for heavier structural studs.
What surface preparation is needed?
Follow the approved procedure. Paint, heavy rust, moisture and other contamination at the weld location can interfere with contact and fusion. A qualified through-deck detail is a separate case from welding through an arbitrary coating.