Selecting weld studs starts with the joint, not a catalog photo. A stud that suits a bridge shear connection may be wrong for a thin electrical enclosure, even if the diameter looks similar. Check the base metal, stud material and geometry, welding process, load, corrosion exposure, and applicable drawing or standard before ordering. This guide follows those decisions from the first specification to production inspection.
What are industrial weld studs?
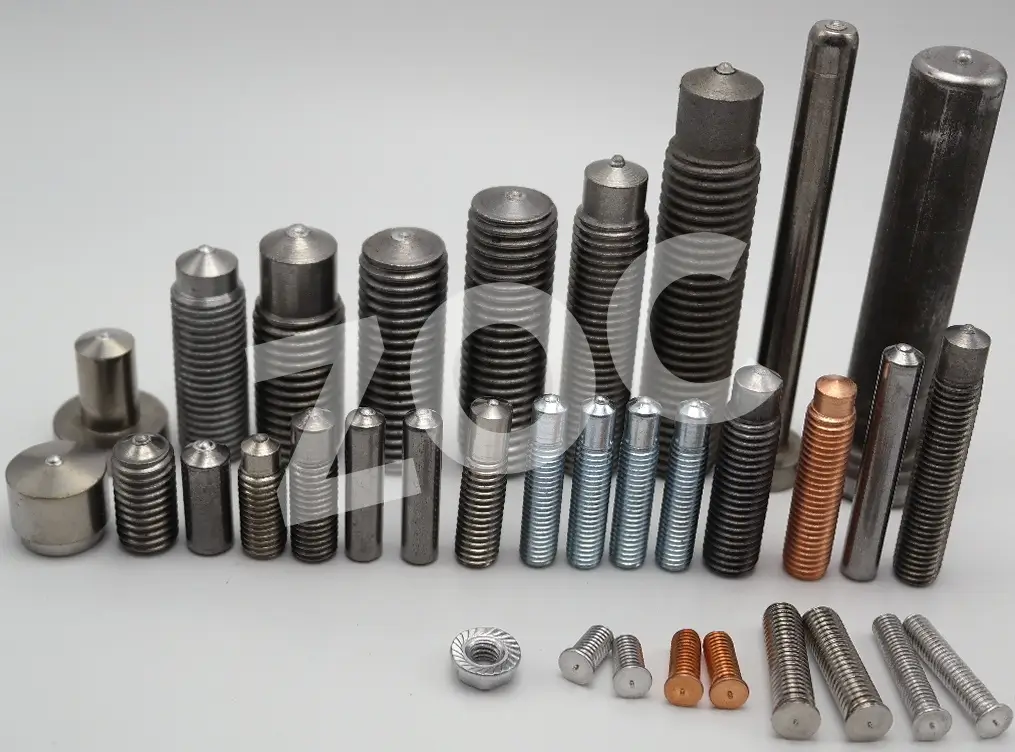
Weld studs are fasteners designed to join to a metal workpiece by stud welding. They can provide a threaded fixing point, a smooth locating pin, an insulation attachment, or a headed shear connector. The weld end is made for a particular process; a threaded rod cut to length is not automatically a substitute. In drawn-arc work, the stud is joined through an electric arc process.
Start with material and geometry
Carbon steel, stainless steel, aluminum, and other alloys appear in stud-welding applications, but the available combinations depend on the process and equipment. Specify the material grade, diameter, length, thread form, weld-end design, and any coating. The base metal and service environment matter just as much as the stud itself.
Our guide to common weld stud types shows the main shapes before you compare individual drawings.
| Specification item | What to record | Why it matters |
|---|---|---|
| Material | Stud and base-metal grades | Weldability and service life |
| Geometry | Diameter, length, thread, and head | Fit and load path |
| Weld end | Tip, flange, or flux design | Process compatibility |
| Finish | Coating or post-weld treatment | Corrosion and weld preparation |
Which drawn-arc weld studs fit the job?
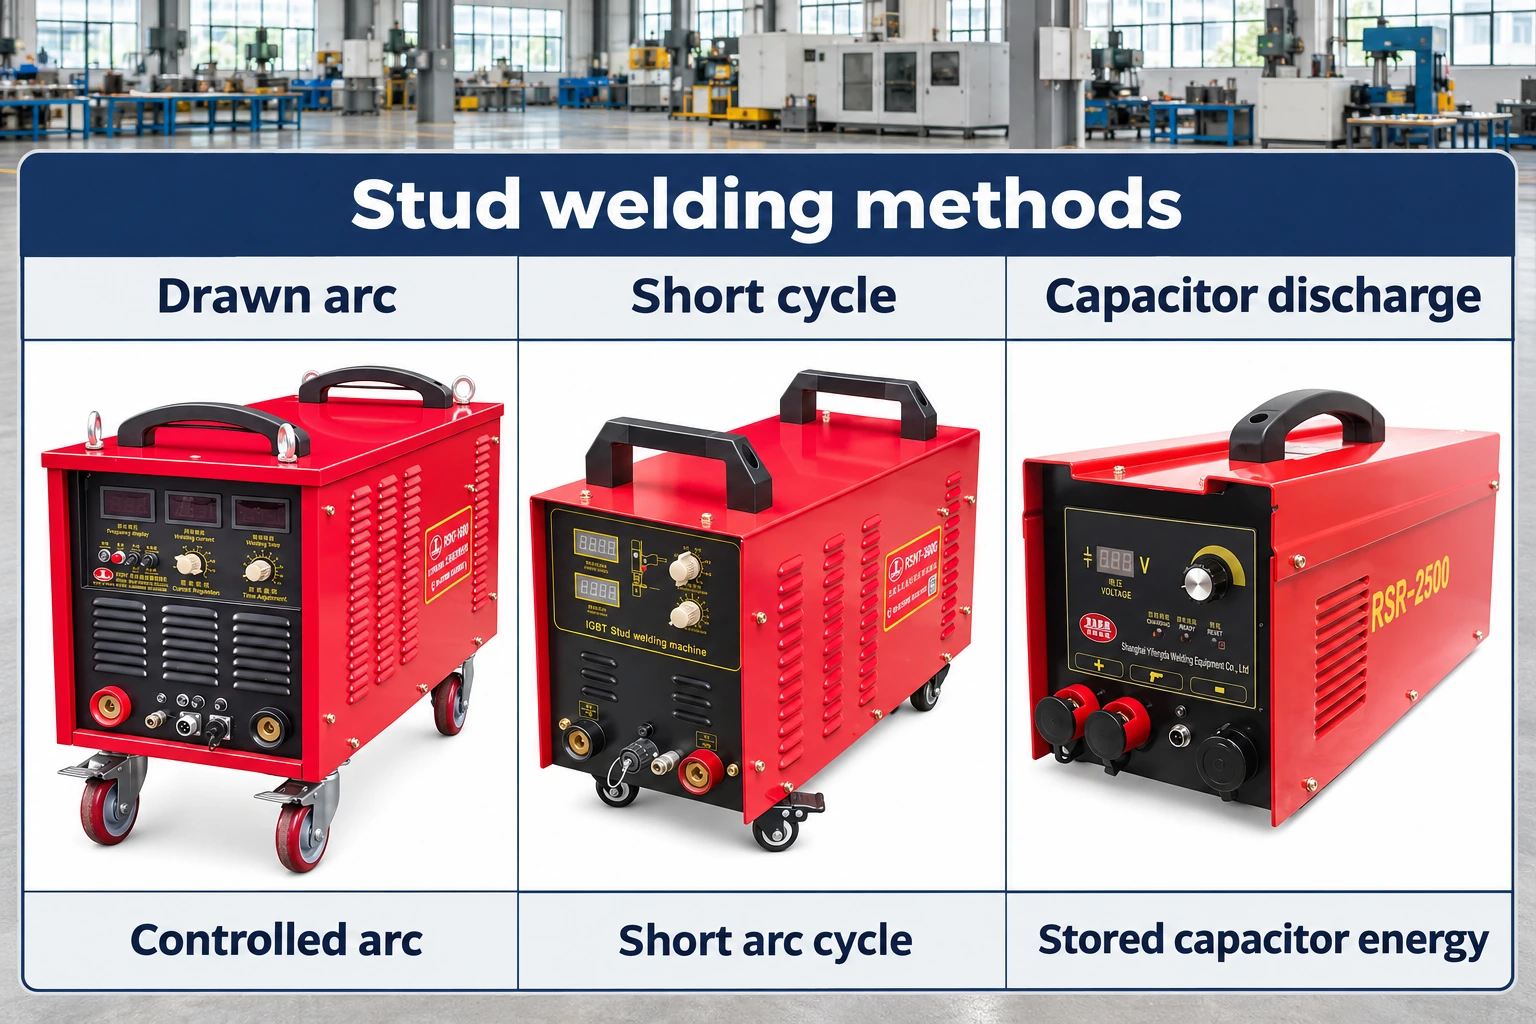
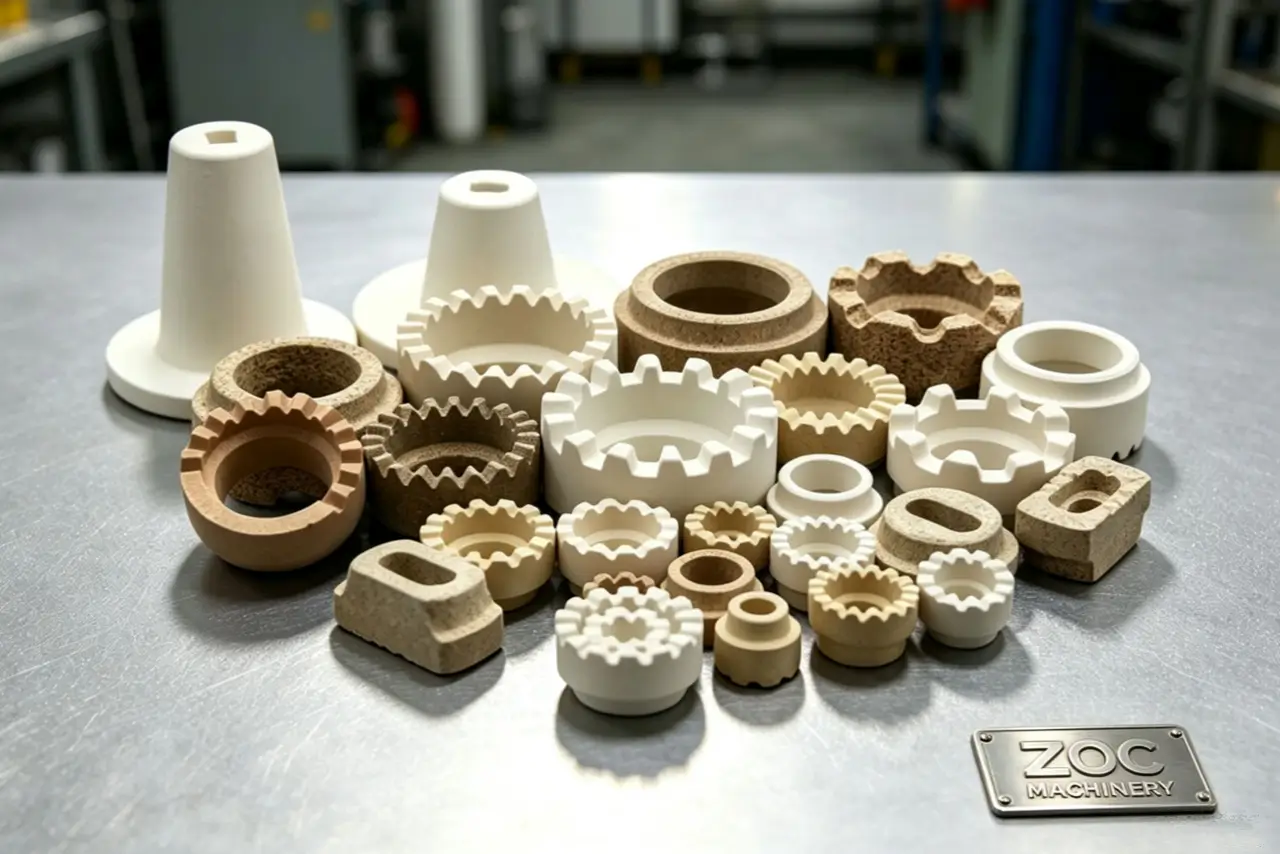
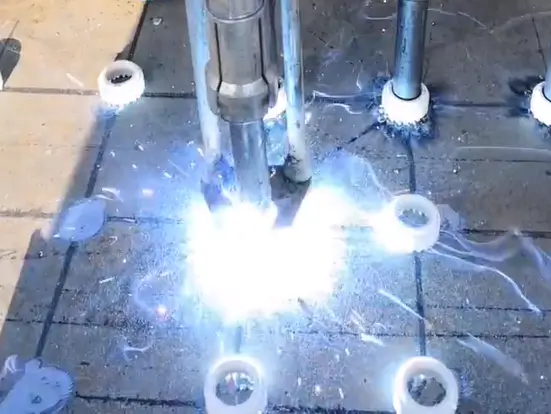
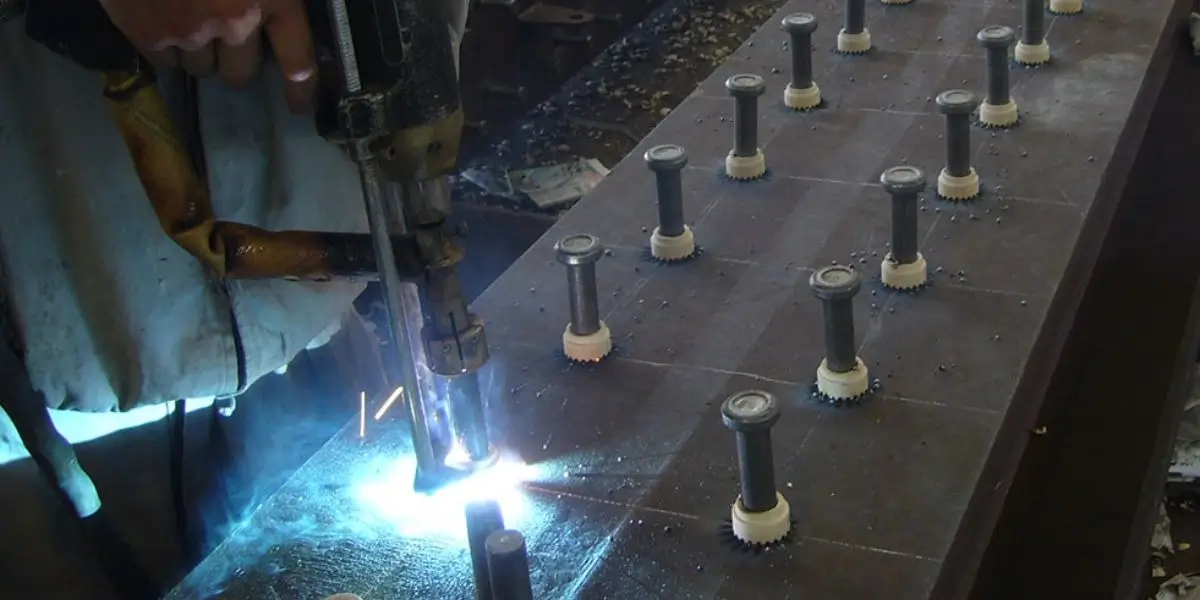
Drawn-arc welding is often chosen for larger studs and structural connections. The gun lifts the stud, an arc melts the joining faces, and the stud plunges into the molten pool. The stud, ferrule or shielding-gas arrangement, gun, power source, and base-metal thickness must work as a system. A ceramic ferrule is common for structural shear connectors, while other approved setups use gas.
Thread and weld-end choices
A fully threaded stud provides adjustment along its length. A partially threaded or unthreaded stud leaves a defined plain shank. A reduced-base design may solve a fit problem, but its dimensions and capacity need checking against the drawing. Thread configuration alone does not establish shear strength or fatigue performance; the whole connection does.
See the arc stud welding process guide for the lift, arc, plunge, and inspection sequence.
| Stud form | Typical reason to specify it | Check before ordering |
|---|---|---|
| Fully threaded | Adjustable fastened assembly | Thread length and weld-end design |
| Partially threaded | Plain shank at a defined location | Grip length and load path |
| Unthreaded | Pin, locator, or insulation attachment | Diameter and retention method |
| Headed connector | Composite steel-concrete connection | Structural design and procedure |
When do CD weld studs make sense?
Capacitor Discharge (CD) weld studs use a short discharge and a purpose-made ignition tip. They are often considered for thinner sheet metal, enclosures, and visible panels because heat input is relatively low. That does not guarantee an unmarked reverse side or a sound weld on every sheet. Material, thickness, surface condition, stud size, and the selected CD method still need trials.
Choose the sheet and stud together
Check whether the sheet can accept the chosen stud without unacceptable distortion or reverse-side marking. The gun, cable arrangement, and charging setting must suit the material. A polished or coated panel also needs a preparation plan at the weld location; do not assume the process can weld through finish without consequences.
For a direct process comparison, read capacitor discharge versus drawn arc.
| Selection point | CD stud consideration | Confirm by |
|---|---|---|
| Sheet thickness | Heat and deformation sensitivity | Trial weld on the actual sheet |
| Stud material | Compatibility with the base metal | Supplier data and procedure |
| Visible face | Acceptable marking and finish | Sample inspection |
| Joint load | Required strength in service | Design and test criteria |
Shear studs in steel construction

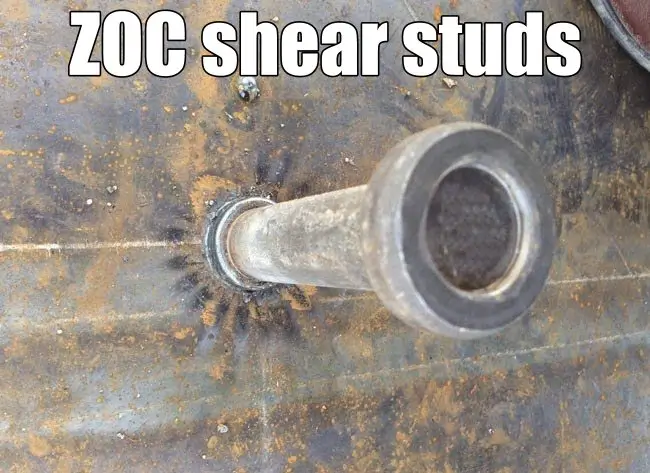
Headed shear studs connect steel beams and concrete slabs in composite construction. Their job is to transfer force across the steel-concrete interface as specified by the structural design. The right choice depends on the stud grade and dimensions, beam and deck arrangement, concrete details, welding procedure, and inspection plan. A visually complete collar alone is not a structural acceptance test.
What the drawing should settle
- Stud diameter, height after welding, grade, and required head dimensions.
- Stud spacing, edge distances, and any deck-through-welding detail.
- The applicable fabrication code and procedure qualification.
- Production inspection and repair instructions.
Our shear studs versus other weld studs guide explains why these connectors should not be selected as ordinary threaded fasteners.
| Component or requirement | Role in the joint | Source of acceptance |
|---|---|---|
| Headed shear stud | Transfers shear in a composite member | Structural drawing and code |
| Base steel and deck | Provides the weld location and geometry | Project specification |
| Ferrule or shielding | Supports the specified weld procedure | Procedure and supplier data |
| Finished weld | Meets production quality requirements | Inspection and test plan |
Weld studs for automated feeding
Automated stud-welding lines need studs that feed and present consistently. A burr, bent shank, uneven flange, or loose flux ball can interrupt the feed path or change the weld position. The useful tolerance is the one required by the feeder and drawing; a blanket claim about micrometre accuracy or welds per minute says little about a particular line.
Trial the complete feeding path
Give the supplier a drawing, the orientation and feed method, and the expected lot size. Run sample studs through the bowl, tube, gun, and weld station before approving volume supply. Record jams, misfeeds, and weld-test results. Automation can improve repeatability, but it does not remove the need to monitor the weld process.
| Check | Manual operation | Automated operation |
|---|---|---|
| Stud presentation | Operator places or loads stud | Feeder and gun must orient it |
| Dimensional variation | May be noticed by the operator | Can stop the feed path |
| Process monitoring | Operator checks output | System data still needs review |
| Changeover | Gun and settings adjusted | Feeder tooling may also change |
Cable-management and attachment studs
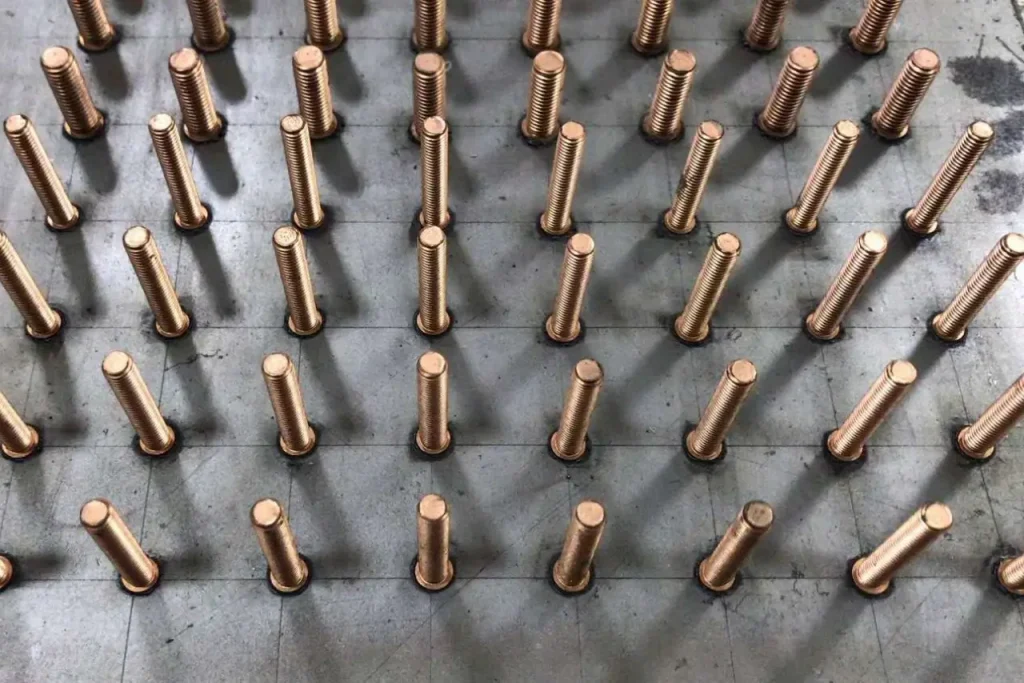
A welded stud can give a chassis, frame, or enclosure a fixing point without a through-hole. Cable ties, clips, brackets, and stand-offs may attach to it, depending on the hardware. Specify the routing load, vibration exposure, electrical requirements, and maintenance access before choosing the stud. A grounding point in particular needs an electrical design and continuity check, not just a mechanical weld.
Match the mount to the service condition
A wire-tie mount needs enough retention for the harness and its environment. A stand-off sets spacing and clearance. A grounding stud requires the correct contact surfaces and testing after coatings or paint are applied. Those are different jobs, even when they use similar-looking studs.
| Mount | Typical use | Additional check |
|---|---|---|
| Wire-tie mount | Secure a cable or hose route | Retention and abrasion |
| Grounding stud | Provide an electrical connection | Continuity and corrosion |
| Stand-off stud | Hold a component away from a panel | Clearance and bending load |
Welded ports and hydraulic assemblies
A weld-on hydraulic port is a different engineered component from an ordinary fastening stud. If a drawing calls for a welded port or threaded boss, evaluate it as part of the pressure boundary. The joint design, material, welding procedure, pressure rating, and leak test must be specified for the whole assembly. A fitting size by itself cannot establish a safe pressure rating.
Questions before approving a weld-on port
- Is the component intended by its manufacturer for this weld process and base material?
- What pressure, temperature, fluid, and fatigue conditions does the assembly see?
- How will weld distortion, thread fit, and leak tightness be checked?
- Which code or customer specification governs qualification and testing?
| Design item | Why it matters | Evidence to request |
|---|---|---|
| Pressure duty | Sets the assembly requirement | Rated drawing and test plan |
| Port material | Affects weldability and corrosion | Material certificate |
| Thread and seal | Controls fitting compatibility | Dimensional and seal specification |
| Completed weld | Must hold under service conditions | Qualified procedure and leak test |
Flux-ball fixing for structural studs
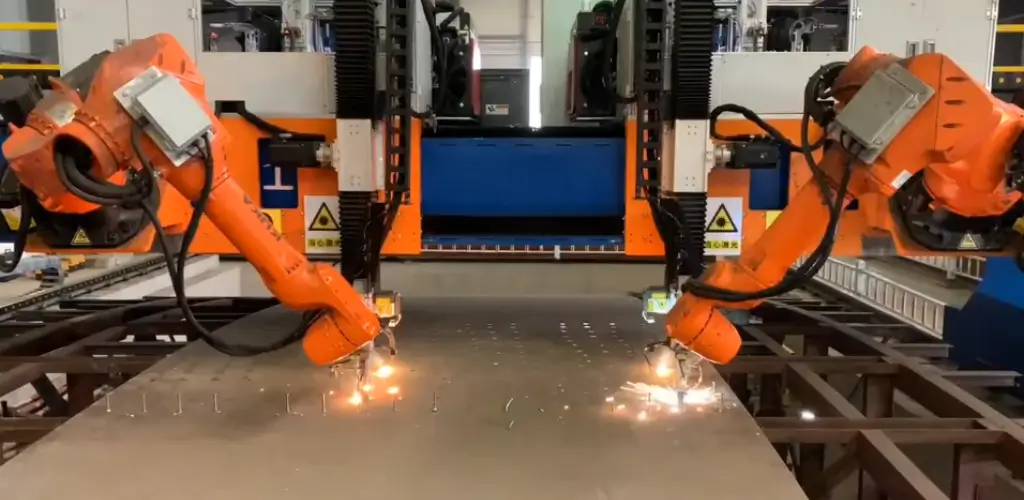
Some drawn-arc shear studs use an aluminum flux ball at the weld end. A fixing machine places and secures that ball before the studs are packed and sent to the welding site. The practical aim is a consistent position and retention, not a guarantee that every subsequent field weld will pass. Stud material, ferrule, surface preparation, equipment settings, and operator technique still affect the weld.
Check the process, not a headline speed
Ask how the flux ball fixing machines are set up for the stud range, how ball presence and retention are checked, and how rejected pieces are handled. The actual throughput and quality rate should be demonstrated on the ordered stud design. Our shear-stud flux fixing machine guide covers the production step in more detail.
| Control point | What to inspect | Why |
|---|---|---|
| Ball position | Centered to the specified design | Consistent starting geometry |
| Retention | Ball remains in place during handling | Reduces missing consumables |
| Stud dimensions | Matches drawing and feeder needs | Fit and weld setup |
| Batch traceability | Lot and inspection records | Follow-up if defects occur |
Standards and weld stud quality checks

The standard named on the drawing determines what to supply and test. ISO 13918 covers dimensions, materials, and mechanical properties of studs and ceramic ferrules for arc stud welding. ISO 14555 covers arc stud-welding procedures, qualification, and production testing. For structural steel work, the contract may also invoke AWS D1.1 or another governing code. These documents have different jobs; a stud certificate does not replace a qualified welding procedure.
Ask for evidence that matches the requirement
When buying weld studs, request the applicable drawing and material or inspection records. For production welds, check the procedure, operator qualification where required, trial-weld results, and the project’s visual and mechanical test criteria. Our stud weld quality guide outlines the shop-floor checks.
| Document or test | What it establishes | Who should confirm it |
|---|---|---|
| Stud drawing and certificate | Material and dimensions | Purchaser and supplier |
| Welding procedure | Approved equipment and settings | Welding coordinator |
| Trial and production tests | Weld behavior on actual work | Inspector per project plan |
| Traceability record | Which batch went into the job | Production and quality teams |
How to choose a weld stud supplier
Send the supplier the drawing and application details before asking for a price. A useful quote identifies the stud grade and dimensions, weld-end type, ferrule if needed, quantity, packaging, inspection records, and lead time. Ask for samples when the stud is new to your equipment or a feeder. The cheapest unit price can become expensive if the studs jam, arrive untraceable, or fail the required procedure trials.
Compare the offer against your specification
- Can the supplier show the requested material and dimensional records?
- Will the stud and ferrule match the approved welding system?
- Can samples be provided for feed and weld trials?
- Are packaging, batch identification, replacement, and delivery terms clear?
For larger orders, the bulk weld stud procurement guide covers lot planning and landed-cost checks. ZOC Machinery can discuss a proposed stud and process when you share the drawing and base-metal details.
| Supplier check | Evidence worth requesting | Decision it supports |
|---|---|---|
| Specification match | Drawing review and samples | Fit and weldability |
| Quality control | Material and inspection records | Batch acceptance |
| Technical support | Process and consumable compatibility | Trial-weld setup |
| Delivery | Lead time and packaging plan | Production scheduling |
Frequently asked questions
Can stainless steel studs be welded to mild steel?
Some combinations are feasible, but the stud, base metal, process, and service environment need a qualified procedure. Consider corrosion of the finished assembly as well as weldability.
How do I reduce spatter?
Check surface condition, ferrule or gas selection, stud geometry, and the lift and plunge setup of the welding gun. Use trial welds to find the cause rather than changing several settings at once.
Can a failed stud be welded again?
Follow the approved repair procedure. A previously fired stud may have an altered weld end and should not be reused as though it were new. The base metal may also need preparation before a replacement is welded.
What process suits thin sheet metal?
Capacitor-discharge welding is often a candidate because of its short cycle and relatively low heat input. Confirm the choice on the actual sheet, stud, and finish; reverse-side appearance is not guaranteed.
How do I know the settings are right?
Use the equipment and stud supplier’s starting data, then inspect and test trial welds under the governing procedure. Fillet appearance helps spot problems, but it is not the only acceptance criterion.
Specify the stud before you buy
A clear drawing and a trial on the real base material settle more than a generic stud catalog can. List the load and environment, choose the matching stud and welding process, then agree on the records and tests required for acceptance. If you need help matching the stud, equipment, and consumables for a particular job, contact us with the drawing, base-metal grade, and planned quantity.