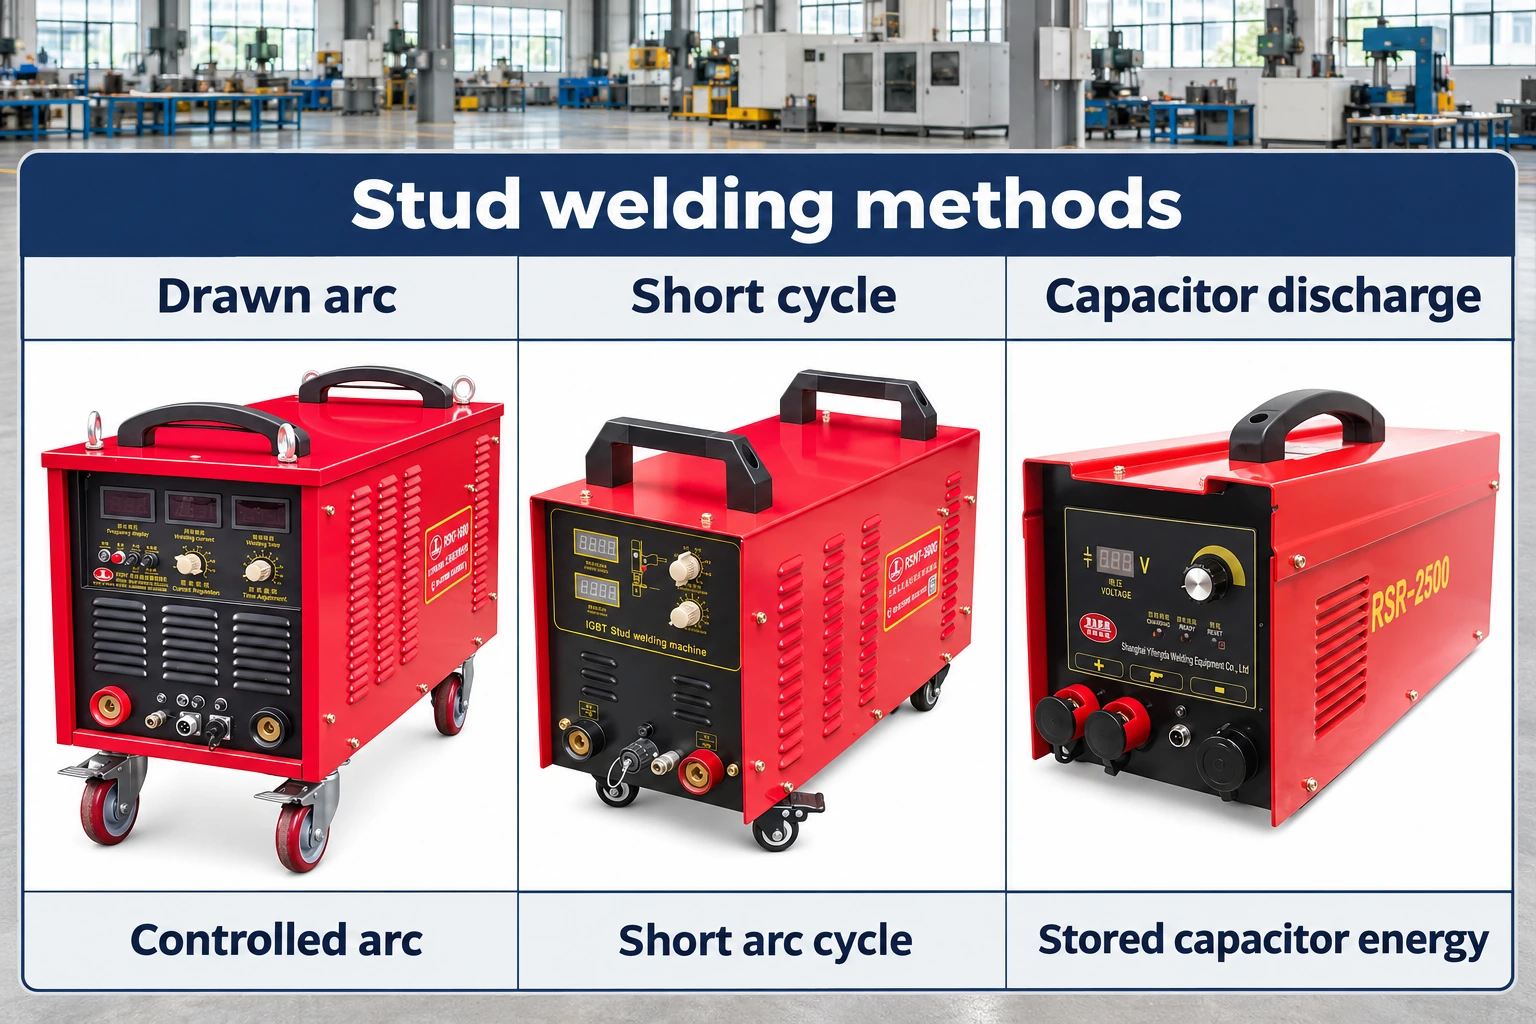
A stud welding gun holds the stud, positions it against the workpiece and controls its movement during the weld. The power source supplies and times the electrical energy. In a drawn arc setup, the gun lifts the stud, the arc melts both surfaces, and the gun plunges the stud into the weld pool. A capacitor discharge (CD) gun can work differently, depending on whether it uses contact or gap ignition.
The gun is only one part of the system. Stud design, power source, cables, return connection, shielding and the base metal all affect the result. This guide explains what the handpiece does, how common gun types differ and what to verify before production.
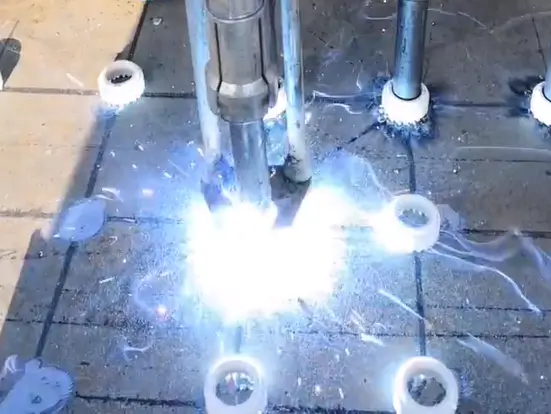
What a Stud Welding Gun Does
The chuck grips the stud and carries current to it. A foot or support keeps the gun aligned with the workpiece. The trigger starts the cycle, while the gun’s internal mechanism moves the stud as required by the process. The power source controls the current and weld time; not every gun has its own display, sensor or programmable controller.
| Gun function | What to check |
|---|---|
| Hold the stud | Chuck fits the stud diameter and weld-end design. |
| Position the weld | Foot and gun can sit squarely at the planned location. |
| Move the stud | Lift and plunge match the selected process and procedure. |
| Carry current | Gun, cable and connectors are rated for the power source. |
A loose chuck or a poor return connection can disturb the weld even when the power-source setting is correct. Check both before changing current or time.
How a Drawn Arc Gun Makes the Weld
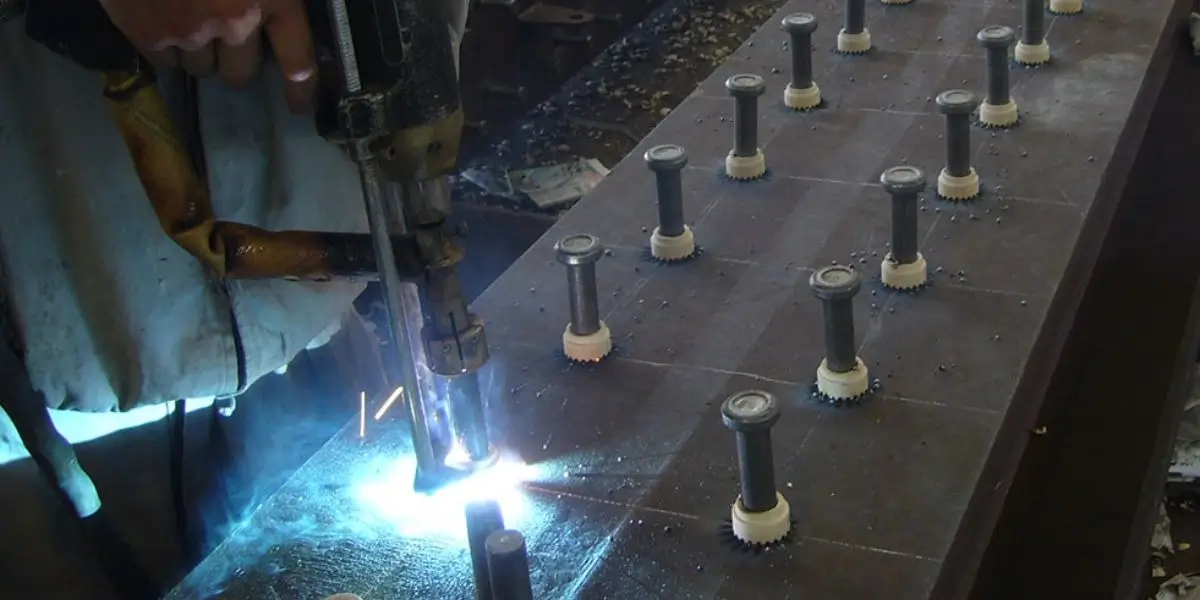
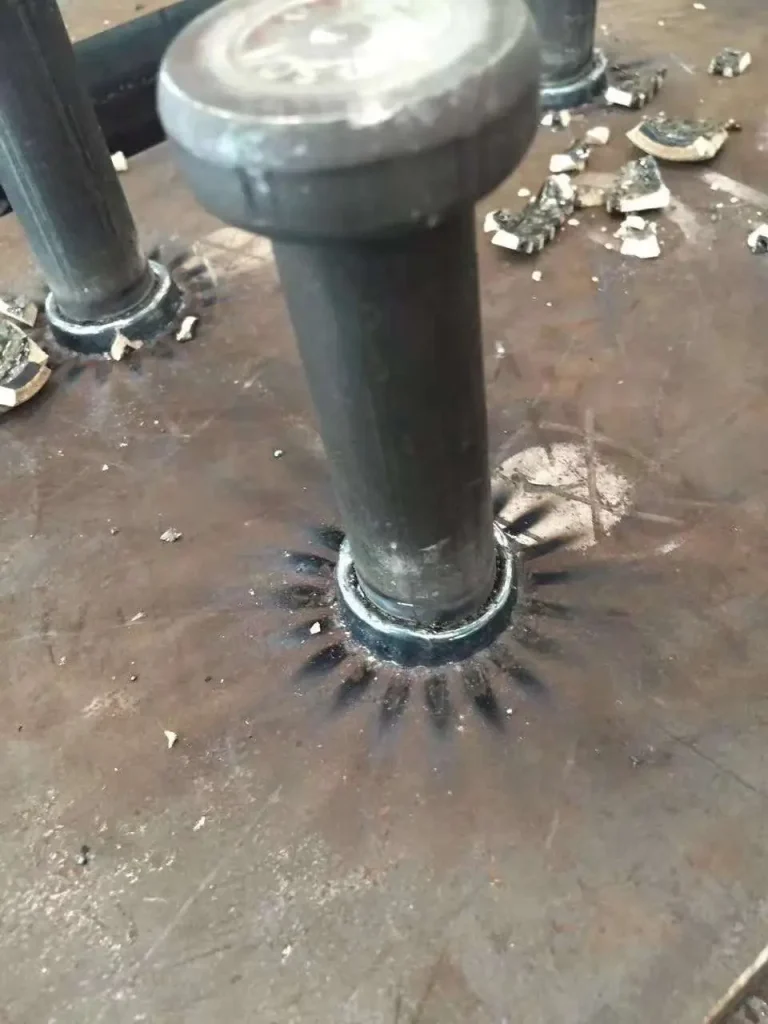
With drawn arc welding, the stud starts in contact with the base metal. After the trigger is pressed, the gun lifts it and an arc forms. The main current melts the stud end and a small area of the workpiece. At the end of the set time, the gun plunges the stud into the molten metal. The joint then solidifies. Our drawn arc stud welding process guide covers the full sequence.
- Seat the correct stud in the chuck and place the gun squarely on the prepared weld point.
- Start the cycle; the gun lifts the stud to establish the specified arc.
- The power source delivers the main current for the set time.
- The gun plunges the stud into the weld pool, then the operator removes the gun after solidification.

| Stage | Gun action | Power-source action |
|---|---|---|
| Start | Holds and lifts the stud. | Starts pilot and main arc as configured. |
| Weld | Maintains the set position. | Controls current and weld time. |
| Finish | Plunges the stud. | Ends the current so the joint can solidify. |
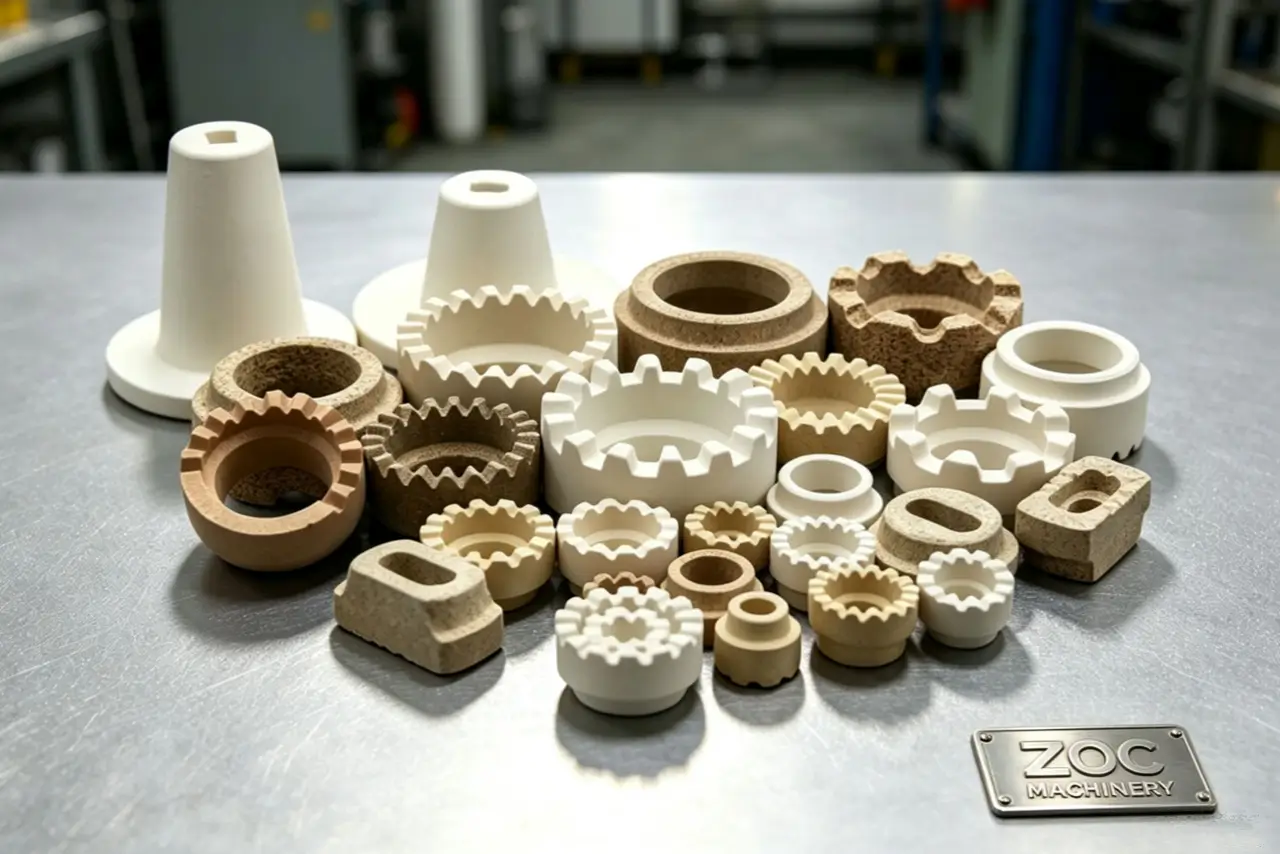
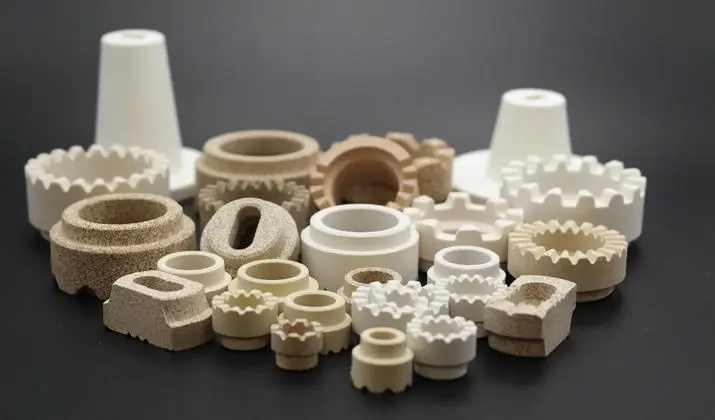
A ceramic ferrule or shielding gas may protect the molten pool, depending on the stud and procedure. The arc does not reliably clean oil, rust or paint from the weld point. Prepare the surface as required and use trial welds to confirm the setup.
Where a Drawn Arc Stud Welding Gun Fits
A drawn arc gun is often specified for larger studs on plate, including headed shear connectors in steel construction. The structural drawing decides the stud and joint requirements; the gun must then match the stud diameter, ferrule or gas setup, cable length and rated current.
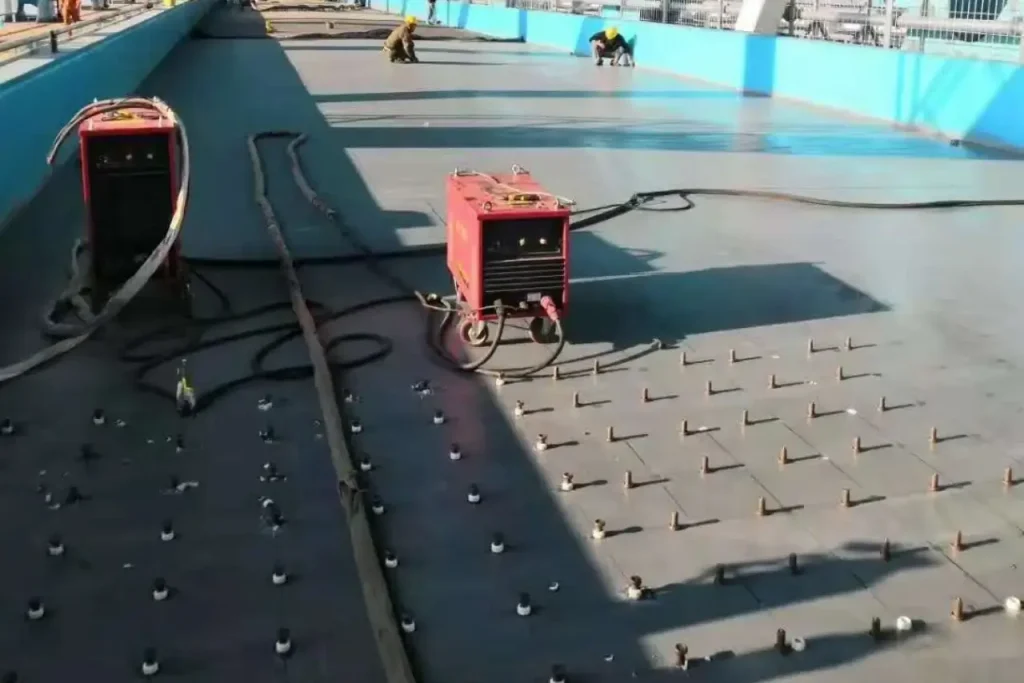
| Selection item | Question for the project |
|---|---|
| Stud size | Is it within the gun, chuck and power-source range? |
| Work position | Can the gun and ferrule sit correctly at each weld point? |
| Power and duty | Can the machine support the current and production rate? |
| Inspection | What tests and records does the project require? |
A long arc does not make every weld stronger than the stud or parent steel. Procedure qualification and production checks establish whether the connection meets the required load.
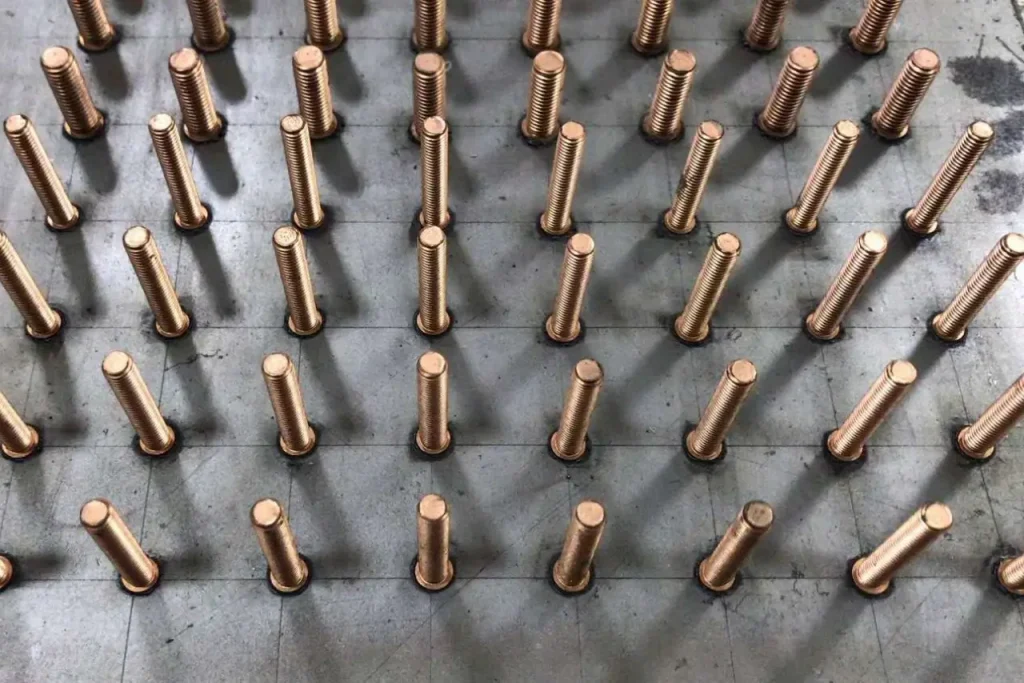
How a Capacitor Discharge Gun Differs
A CD system stores energy in capacitors and releases it in a short pulse. In contact ignition, a spring holds the stud’s ignition tip against the workpiece; the tip vaporizes and starts the arc. In gap ignition, the stud begins above the surface and moves toward it when the cycle starts. These guns do not all use the same lift-and-plunge sequence as a conventional drawn arc gun. See our comparison of CD and drawn arc welding.
| CD method | Starting position | Gun movement |
|---|---|---|
| Contact ignition | Stud tip touches the workpiece. | Spring pressure moves the stud into the molten area. |
| Gap ignition | Stud starts at a set distance above the surface. | Gun accelerates it toward the workpiece. |
| Both methods | Require a compatible stud and clean weld area. | Need the correct chuck, cable and tested setting. |
CD welding is often considered for small studs on suitable thin sheet, where rear-side appearance matters. A short pulse can limit heat input, but it does not guarantee a mark-free panel or a sound weld on every material. Inspect the reverse side and test the joint on a sample part.
The Main Parts of a Stud Welding Gun
The exact construction varies by model. Common parts are the chuck, gun body, trigger, foot or legs, cable and a mechanism that controls stud movement. A drawn arc gun may use an electromagnet for lift and a spring for plunge; a contact CD gun may rely mainly on spring pressure. Check the parts diagram for the model you own.
| Part | Job | Routine check |
|---|---|---|
| Chuck | Grips the stud and transfers current. | Fit, wear and contamination. |
| Foot or support | Keeps the gun aligned and sets its working position. | Damage and correct adjustment. |
| Lift or spring mechanism | Moves the stud in the required sequence. | Travel and freedom of movement. |
| Cable and connector | Carry current and control signals. | Insulation, strain relief and secure connection. |
Built-in sensors, interlocks and displays are model-specific. Confirm those features from the manual or data sheet rather than assuming they are standard on an industrial gun.
Set Up the Gun for a Trial Weld
Start with the stud, base metal and specified process. Fit the matching chuck, inspect the cable and return connection, set the gun according to its manual, and confirm the power-source program. Then weld a representative sample and inspect it before making production parts. The stud welding parameters guide explains current, time, lift and plunge in more detail.
| Setup step | Record before production |
|---|---|
| Stud and chuck | Stud part number, diameter, weld end and chuck size. |
| Gun position | Foot setting, access angle and lift or spring setup. |
| Power source | Program, current or charge setting, weld time and cable length. |
| Trial result | Visual check, required mechanical test and any rear-side marking. |
Avoid copying a voltage or lift distance from a generic chart. The right setting depends on the exact gun, power source, stud and material. If a test weld fails, identify the cause before increasing energy.
Materials and Surface Preparation
Stud guns can be used with mild steel, stainless steel and some aluminum or brass combinations when the stud, power source and procedure support them. Material compatibility is a system question, not a property of the gun alone. Coatings, mill scale and oil can change arc behavior and must be handled by an approved preparation method.
| Material or surface | Selection check |
|---|---|
| Mild steel | Stud grade, plate thickness and weld-point preparation. |
| Stainless steel | Compatible stud and any shielding or corrosion requirements. |
| Aluminum | Process variant, polarity or gap setting and shielding where specified. |
| Paint or zinc coating | Removal or qualified through-coating procedure and fume control. |
Neither CD nor drawn arc automatically preserves the reverse finish of a panel. Weld a sample of the actual sheet and inspect both faces when appearance is part of the acceptance criteria.
Production Speed and Automation
A gun can reduce handling where a design allows a one-sided welded fastener instead of drilling and through-bolting. Arc time is only a small part of the cycle. Loading, positioning, ferrule or gas handling, inspection and rework determine accepted output.
| Production measure | What to compare |
|---|---|
| Complete cycle | Time from picking up a stud to an inspected weld. |
| Accepted output | Good welds per shift, not trigger pulls. |
| Changeover | Chuck, stud, fixture and program changes. |
| Automation | Feeder and robot availability plus stoppages. |
Robotic or CNC mounting can improve repeatability when the part, gun and feed system are controlled. It does not remove the need for procedure qualification, maintenance and inspection. Ask suppliers for a demonstration using your stud and part rather than a generic speed claim.
Safety Checks Before Firing
A brief stud-welding arc still presents eye, skin, fume, burn and electrical hazards. Use the protection specified by the equipment manual and the site safety plan. Keep people out of the arc’s line of sight, control combustible materials and provide ventilation appropriate to the metal and coating being welded.
| Before welding | Check |
|---|---|
| Eye and skin protection | Suitable welding eye protection, gloves and protective clothing. |
| Electrical setup | Intact gun and return cables, secure connectors and dry work area. |
| Hot work area | Combustibles controlled and other workers protected from the arc. |
| Fumes | Ventilation or extraction matched to base metal and coating. |
Do not assume a gun has an interlock that makes an unsafe setup harmless. Stop and isolate the equipment before changing a chuck, inspecting internal parts or repairing a damaged cable.
Maintain the Chuck, Mechanism and Cables
Inspect the chuck for loss of grip, arcing or contamination. Check the gun foot and moving parts for damage, and protect cables from sharp edges and tight bends. Use the model’s service intervals and approved cleaning method; an arbitrary daily brushing or lubrication schedule can damage some designs. Our stud gun maintenance guide covers what to record.
| Item | Inspect for | Action |
|---|---|---|
| Chuck | Wear, heat marks or poor stud grip. | Clean or replace as the manual directs. |
| Gun movement | Sticking, damaged support or incorrect travel. | Adjust or service before production. |
| Power and control cables | Cuts, loose terminals or strained connectors. | Isolate and repair with approved parts. |
| Stored gun | Moisture, impact or contamination. | Store to the manufacturer’s instructions. |
If weld quality changes, compare the current setup with the last accepted trial. The stud weld quality checks guide describes checks for the weld itself; gun maintenance is only one part of that investigation.
Choose a Gun as Part of the Welding System
Start with the process, stud size, material, work position and expected daily output. Then match the gun to the power source, cable arrangement and consumables. You can compare ZOC’s stud welding gun range with its manual stud welding guns and ask for the data sheet of the exact model.
Send a stud drawing, base-metal specification, available electrical supply and acceptance criteria when requesting a configuration. That gives the supplier enough detail to propose a gun, power source and trial plan.
Frequently Asked Questions
Can I weld on a painted surface?
Prepare the weld point as the procedure requires. Paint normally interferes with electrical contact and fusion; through-coating welding needs a qualified setup for that coating and part.
What makes a weld repeatable?
Use the same stud, prepared material, gun setup, power-source program and inspection method. Check the chuck and cables when results change, and record approved settings.
How do I know the plunge setting is right?
Set it by the gun manual and procedure, then make trial welds and inspect or test them to the job requirement. Fillet shape alone cannot prove strength.
Can a CD gun weld large structural studs?
CD equipment is generally selected for smaller studs. Large structural connectors usually call for a specified drawn arc system. Check the structural drawing and the rated range of the exact machine and gun.
How should I store the cables?
Keep them dry, protected from damage and free of sharp bends. Follow the manufacturer’s guidance for coiling, connectors and inspection.
If you need a matched system for your stud and application, contact us with the drawing, material and production requirements.