Stud welding applications range from shear connectors on steel beams to small mounting studs inside electrical cabinets. The appeal is simple: a stud can be attached from one side without drilling a through-hole. The right process and joint design still depend on the stud, base metal, load and inspection requirement.
This guide shows where manufacturers and contractors use welded studs, pins and connectors, and what you should check before choosing equipment. A no-hole attachment can help preserve a panel surface, but it does not by itself prove strength, water tightness or an enclosure rating.
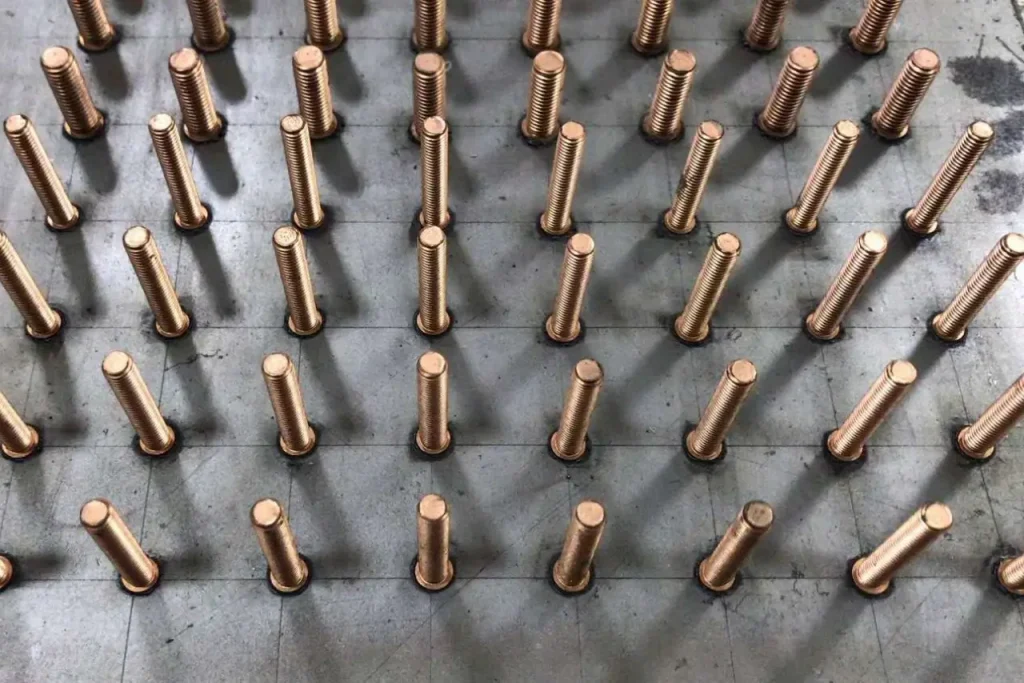
Common Industrial Stud Welding Applications
Different industries use different weld elements. A headed shear stud on a beam, a threaded earth stud in a cabinet and an insulation pin on ductwork do different jobs. Match the element and welding process to the job rather than ordering a machine from a list of industries.
| Application | Typical attachment | First design check |
|---|---|---|
| Steel and composite construction | Headed shear connector on structural steel | Specified load, steel grade and approved weld procedure |
| Vehicle and appliance production | Threaded or flanged mounting stud | Sheet thickness, rear-side appearance and repeatability |
| Electrical enclosures | Grounding point or component standoff | Electrical continuity, material and enclosure design |
| HVAC and industrial insulation | Pin or stud for blankets and cladding | Base-metal thickness, insulation system and service temperature |
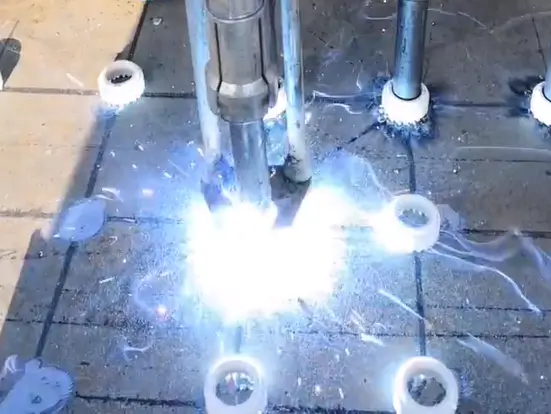
The arc itself is brief, but production time also includes positioning, feeding, ferrule or gas handling and inspection. Compare accepted welds per shift when speed is part of the purchase case.
Automotive and Sheet-Metal Assemblies
Vehicle manufacturers use studs for brackets, wiring and trim attachments where a welded fastener suits the panel design. The attachment has to survive the specified vibration, temperature and corrosion exposure. A good-looking weld is not a substitute for that validation.

| Vehicle area | Possible stud-welded part | What to validate |
|---|---|---|
| Exhaust vicinity | Heat-shield or bracket attachment | Temperature, material pairing and vibration |
| Body or interior panel | Trim or cable fixing | Rear-side marking and coating sequence |
| Chassis assembly | Line or harness support | Required load, fatigue and access for the gun |
Thin sheet often calls for a lower-heat process, but the process name alone will not prevent marking or distortion. Test the actual panel, including any coating and the reverse face, before production.
Steel Construction and Composite Decking
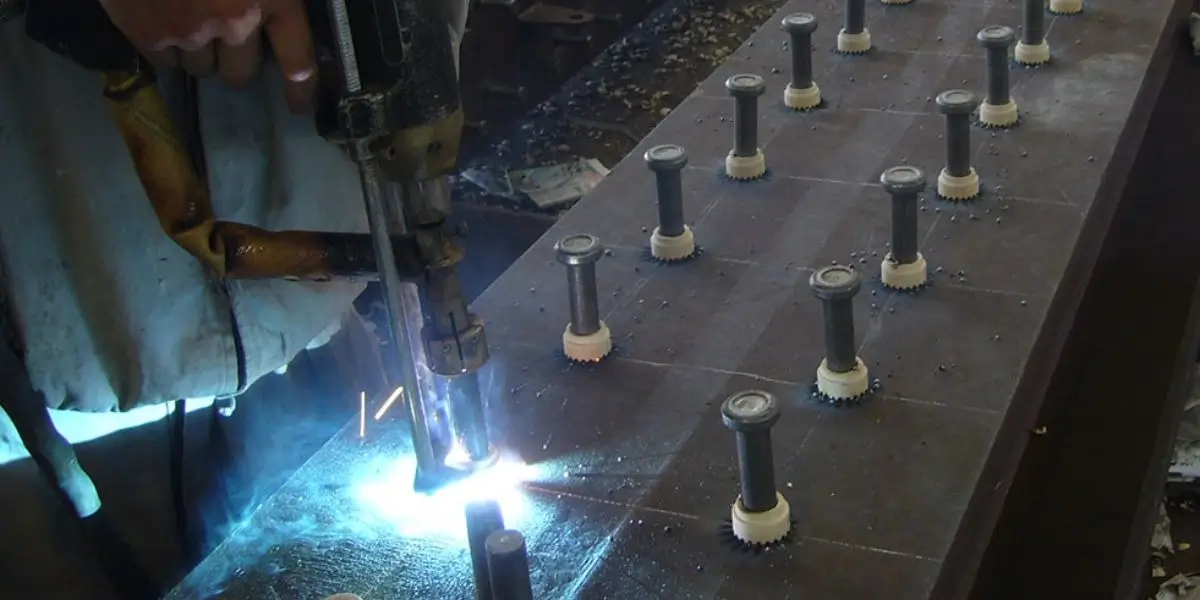
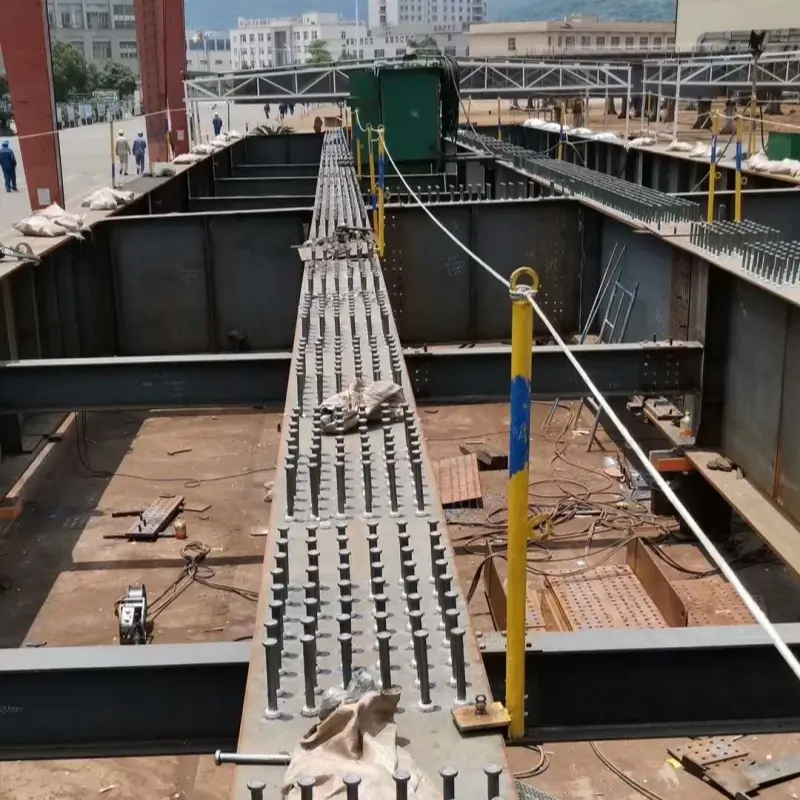
Headed shear connectors join a steel member to a concrete slab so the assembly can act as designed. They are common on composite beams and decks, where stud size, placement and weld quality are set by the structural design. Our guides to shear stud applications in steel construction and shear studs and regular weld studs explain the connector’s role and how it differs from a general-purpose fastening stud.
| Construction task | Stud or connector | Critical check |
|---|---|---|
| Composite beam or deck | Headed shear stud | Drawing, spacing, base-metal condition and weld procedure |
| Bridge component | Specified structural connector | Project detail, access and production testing |
| Secondary bracket | Approved welded stud or fitting | Load path and whether welding is permitted on the member |
Do not assume every welded stud is a shear connector. Structural studs are selected for a defined load path and require the procedure and inspection specified for the project. Site power, cable length and weather also affect equipment selection.
Choose the Process for the Stud and Base Metal
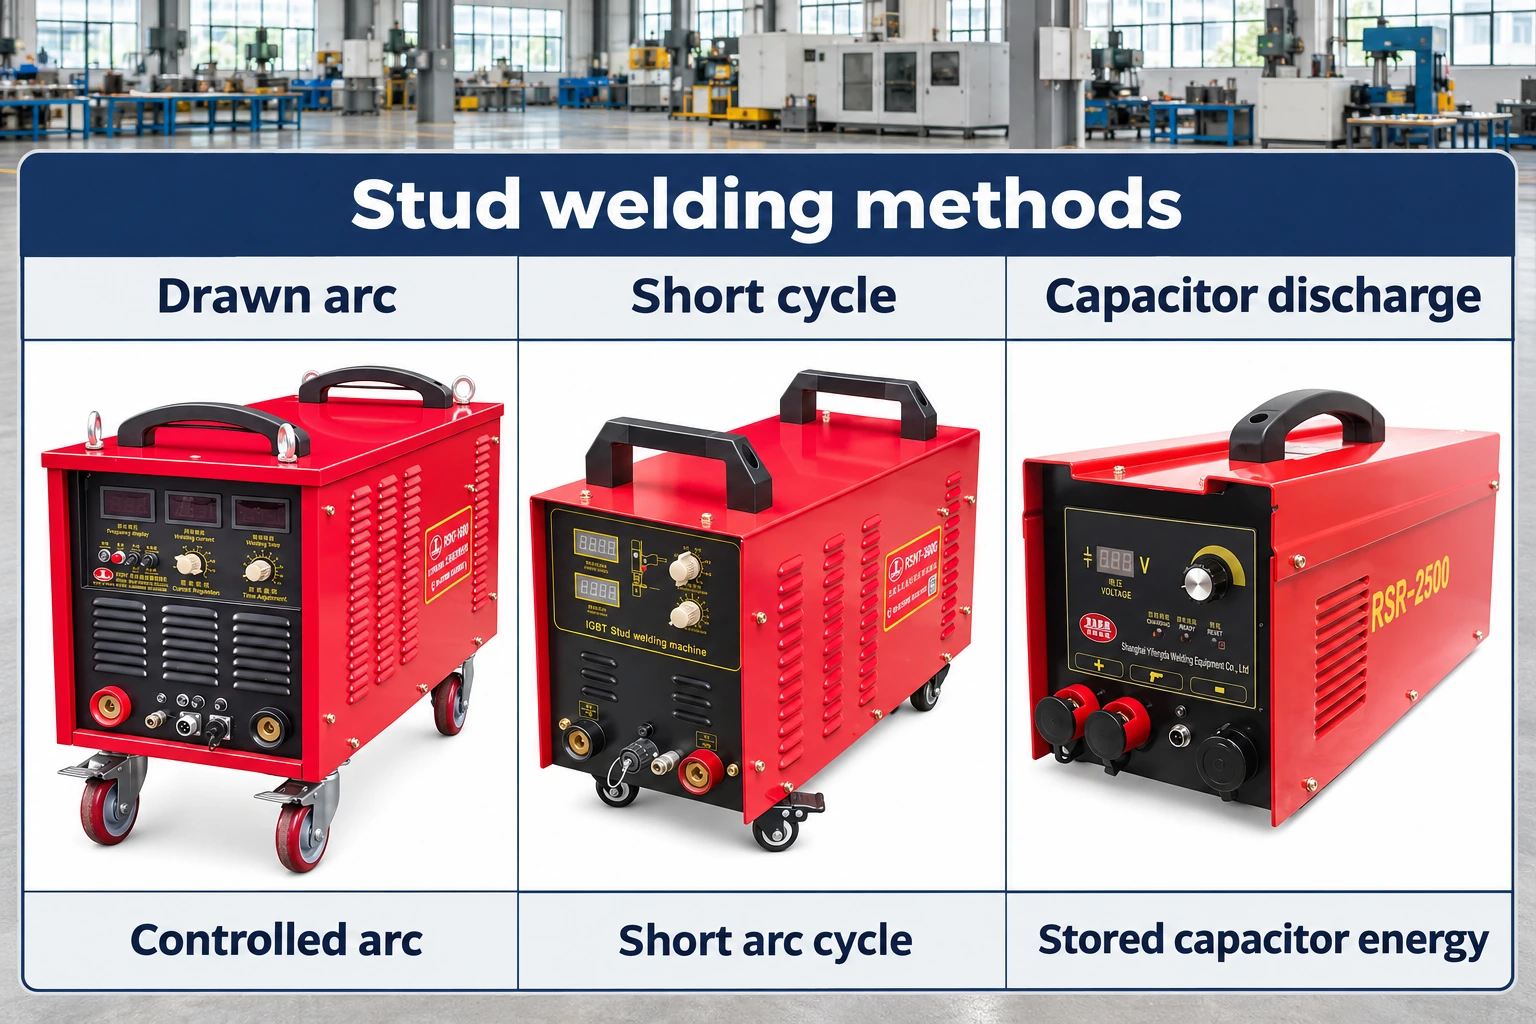
Capacitor discharge, short cycle and conventional drawn arc welding cover different stud sizes, weld-end designs and material combinations. Compare CD and drawn arc stud welding when thin sheet and larger studs are both in the discussion. Our short cycle and drawn arc guide looks at the arc-time choice within drawn arc welding.

| Process | Common starting point | Verify before selection |
|---|---|---|
| Capacitor discharge | Small studs and suitable thin sheet | Stud tip, base metal and reverse-side finish |
| Short cycle drawn arc | Repeat sheet-metal work with a compatible stud | Stud size, shielding and trial-weld result |
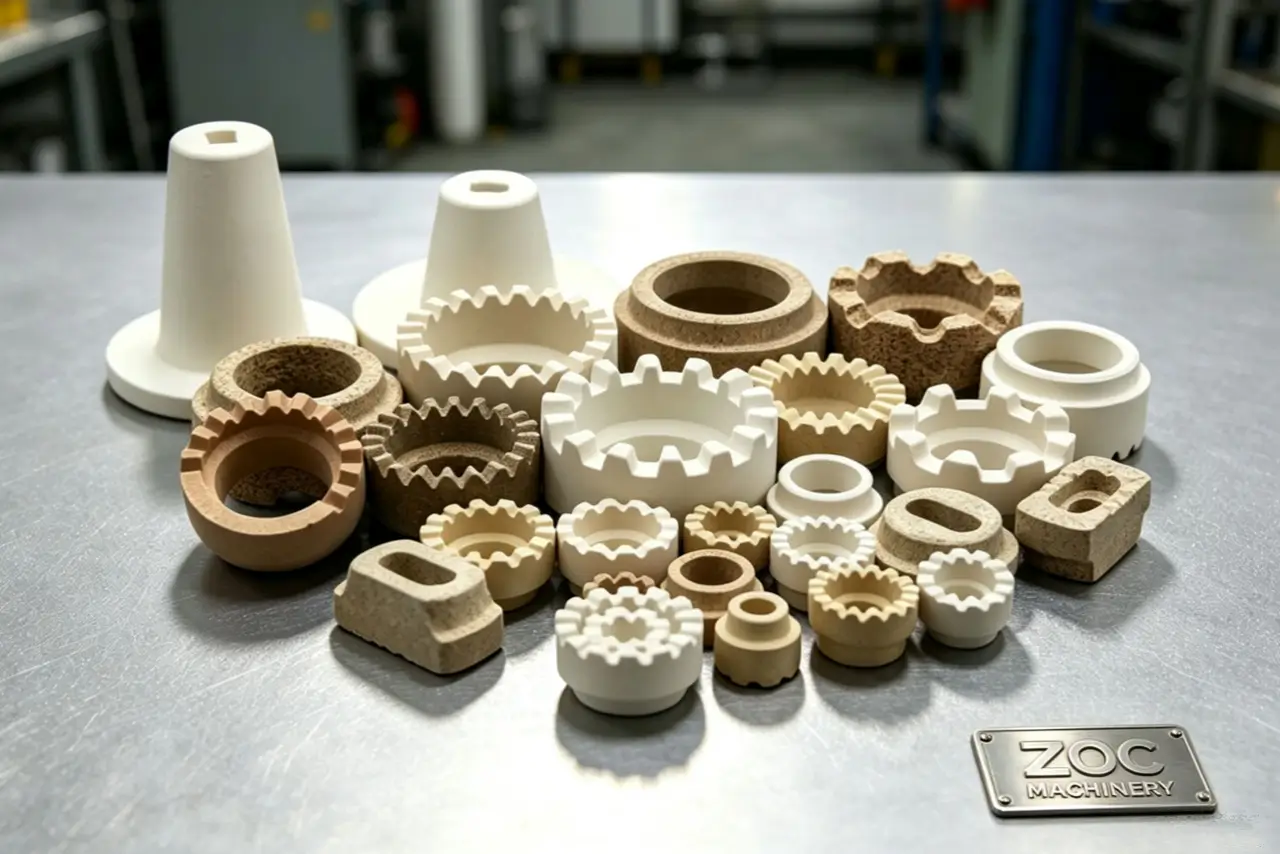
| Conventional drawn arc | Larger studs and structural work | Ferrule or gas, rated output and project procedure |
There is no universal plate-thickness chart that replaces a model data sheet or trial weld. Set current, time, lift and plunge for the stud and material, then check the joint against the acceptance criteria. The stud welding parameters guide explains what each setting changes.
Building Facades and Cladding
Welded studs can provide concealed attachment points behind a metal facade or cladding panel. The designer still needs to account for wind load, panel movement, corrosion and the way the bracket or rail transfers force to the structure.

| Cladding concern | What a welded stud can do | What it does not guarantee |
|---|---|---|
| Visible finish | Hide a fixing behind a panel | A mark-free front face without a sample test |
| Weather exposure | Avoid a through-hole at that attachment | A waterproof facade without a complete seal design |
| Thermal performance | Change the fixing detail | Elimination of thermal bridging or condensation |
A no-hole fastening detail can be useful, but weatherproofing and insulation depend on the entire wall assembly. Confirm the stud location and weld procedure with the facade engineer rather than treating the stud as a replacement for the building-envelope design.
Electrical Cabinets and Equipment Enclosures
Small studs and bosses can mount components, cable supports and grounding terminals inside metal cabinets. CD welding is one option on suitable sheet; the enclosure material, stud design and electrical requirements decide whether it is appropriate.

| Cabinet need | Possible attachment | Check |
|---|---|---|
| Protective earth | Specified grounding stud or terminal | Continuity, corrosion and approved electrical connection |
| Component mounting | Threaded stud or standoff | Stud load and clearance to live parts |
| Outdoor enclosure | Interior welded fixing | Full enclosure seal and tested ingress rating |
A welded stud does not automatically give an enclosure an IP rating or make a ground connection compliant. Check the complete enclosure and electrical assembly under the applicable specification.
HVAC, Boilers and Industrial Insulation
Insulation pins are welded to ducts, tanks and other metal shells to hold blankets or cladding with washers. The pin, weld and insulation must suit the substrate and service temperature. Thin duct sheet needs a different setup from a thick boiler shell.

| Insulation job | Typical fastener | Check |
|---|---|---|
| HVAC duct | Insulation pin or cup-head pin | Sheet thickness, backside appearance and blanket load |
| Boiler or vessel | Rated stud or pin | Service temperature, access and approved procedure |
| Acoustic lining | Pin with retaining washer | Vibration and lining-system requirements |
A welded pin can remove the need for a drilled fastening point, but it does not guarantee blanket life. Specify the washer, insulation and corrosion protection as one system.
Energy and Plant Equipment
Power plants and other industrial sites use welded attachments for insulation, cable supports, instruments and access components. Renewable-energy equipment can use similar details, but the fastening method must come from the project design; a solar frame or wind tower is not automatically a shear-stud application.

| Plant location | Possible use | Project check |
|---|---|---|
| Tower or equipment enclosure | Cable or instrument support | Fatigue, corrosion and permission to weld |
| Solar support structure | Specified bracket attachment | Base-metal grade and structural approval |
| Pipe or vessel shell | Insulation or sensor support | Pressure-boundary rules and heat input |
Never add a stud to a pressure boundary or fatigue-critical member on the basis of a general application guide. Obtain approval for the location and use the required welding and inspection procedure.
Shipbuilding and Marine Fabrication
Shipyards use welded studs and pins to support cables, pipework, insulation and interior fittings. One-sided access can help on large plates and bulkheads. It does not by itself establish a watertight or fire-rated boundary.

| Ship area | Possible attachment | Check |
|---|---|---|
| Bulkhead | Cable or pipe support | Location approval and required fire or water rating |
| Hull or deck insulation | Pin or stud for cladding | Material, coating and corrosion protection |
| Interior fitting | Threaded mounting stud | Load, access and inspection method |
Marine material choices and coating repairs matter after welding. Confirm that the welding detail is permitted on the plate and that any compartment rating is assessed for the complete assembly.
Maintenance, Retrofitting and Field Work
A portable inverter stud welder can help fit a new bracket or support where the workpiece cannot be moved. Repair work needs more than a fast arc: identify the parent metal, old coating, available power and the load on the new stud.
| Field task | Potential advantage | Required check |
|---|---|---|
| Replace an attachment | Work from the accessible side | Condition of the base metal and repair approval |
| Add a sensor support | Avoid a through-hole | Heat-sensitive equipment and electrical isolation |
| Fit a bracket | Limit disassembly | Load, fit-up and inspection access |
Do not weld over a failed fastener without finding why it failed. For load-bearing repairs, use the approved repair procedure and record the result. Our stud weld quality checks article covers checks to discuss before accepting production or repair welds.
What to Specify Before Ordering Equipment
Send the stud drawing, base-metal grade and thickness, coating, required load, access conditions and production volume. State whether appearance, corrosion, electrical continuity or a structural code governs the joint. Those details let a supplier propose a process and a trial weld instead of choosing by industry name alone.
If you need a machine and gun configuration, contact us with the part details and the inspection requirement. Ask for the supported stud range, consumables and service parts in the same quote.
Frequently Asked Questions
Is CD welding always best for thin sheet?
No. It can be a good option for small studs on suitable sheet, but stud design, surface condition, load and rear-side finish decide the setup. A trial weld answers more than a process label.
Can studs be welded through paint or zinc?
Only when the procedure covers that surface and the weld passes testing. Coatings can change arc behavior, produce fumes and affect the joint. Prepare the weld area as specified rather than assuming the arc will clean it.
Does no through-hole mean a leak-proof enclosure?
No. The attachment avoids a hole at that point, but seals, other penetrations, corrosion and the full assembly determine leak tightness or an IP rating.
How fast is a stud weld in production?
The arc is brief. Total production time includes loading, locating the part, moving the gun, any ferrule or gas handling and inspection. Compare accepted output for the actual job.
Does a welded stud weaken the base metal?
Welding changes a local area of the base metal. Whether that is acceptable depends on the joint design, material, procedure and testing. Do not assume every stud weld is stronger than the stud or parent plate.