Choosing a Stud Welding Machine for steel structure construction starts with the stud on the drawing. A power source that handles one shear connector may not suit a larger stud, a different gun, or through-deck welding. Before comparing prices, note the weld-base diameter, steel grade, deck profile, welding position, site power, and required inspection.
Start with the Structural Connection
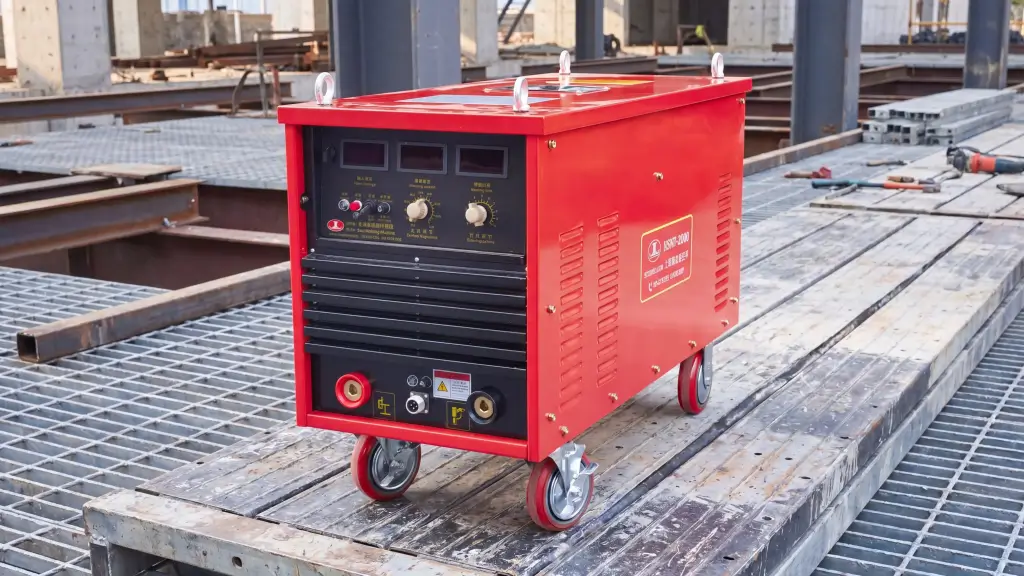
A structural stud welder must make repeatable welds with the specified studs and base metal. The machine rating matters, but so do the gun, cable length, return connection, ferrule, surface condition, and welding procedure. A larger current number alone is not proof of a sound connection.
Why the Connector Weld Matters
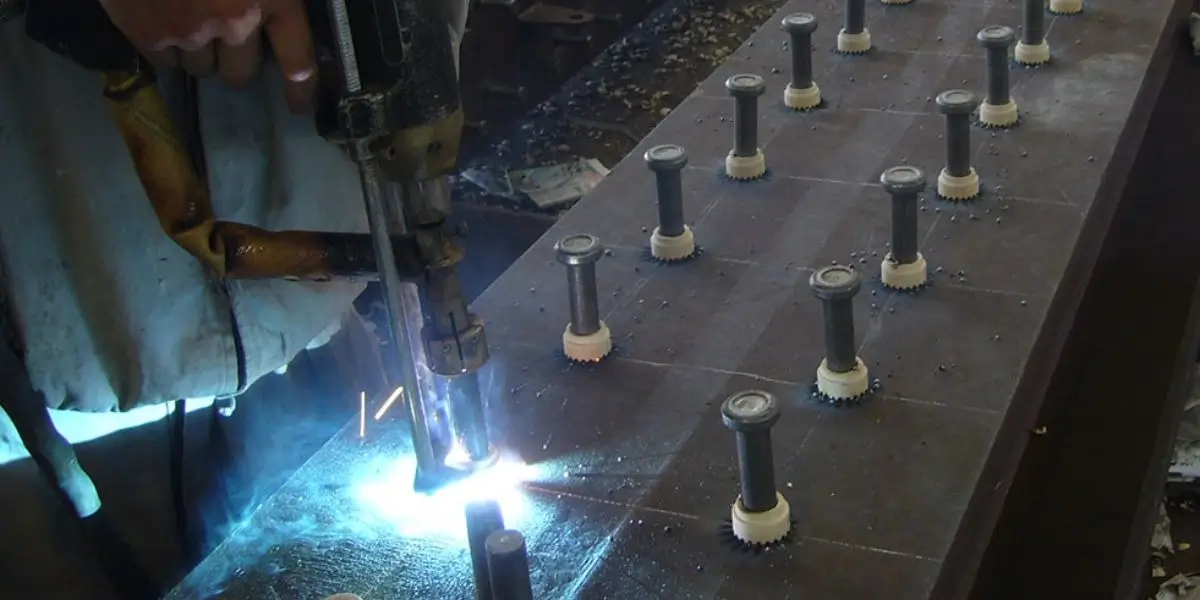
Composite floors use headed shear connectors to transfer force between the concrete slab and steel beam. The weld at the base of each connector is part of that load path.
A poor weld can require repair or replacement and interrupt decking work. Start with the approved connection detail, then choose a process and machine able to make it.
- Weld quality depends on the approved procedure and correct setup.
- Heat input must suit both the stud and the base metal.
- Inspection confirms whether the joint meets the project criteria.
Stud welding is useful when many connectors must be placed along beams or through decking. Its short weld cycle can help production, although positioning, ferrule handling, testing, and moving between locations take additional time.
How the Process Fits a Site Schedule
The arc itself is only one part of the cycle. An operator still positions the welding gun, checks the ferrule and return connection, makes the weld, and inspects the result.
Surface preparation also matters. Remove contamination as the approved procedure requires; do not assume a high-current machine can weld reliably through paint, oil, or heavy scale.
Choose the equipment for the specified joint and the rate your crew must sustain, not for a promised percentage of labor savings.
When comparing installation methods, include setup, inspection, ferrule removal, access, and repairs in the time estimate.
| Buying check | Drawn arc stud welding | Other approved attachment method | What to measure | Why it matters |
|---|---|---|---|---|
| Stud placement | Short arc cycle plus handling | Process-specific setup and weld time | Accepted studs per shift | Arc time is not crew time |
| Joint acceptance | Per stud procedure | Per alternate design and procedure | Test and repair results | Compare the same joint requirement |
A fast weld cycle helps only when the crew can position and check each connector at the required quality.
Match the Machine to the Stud and Base Metal
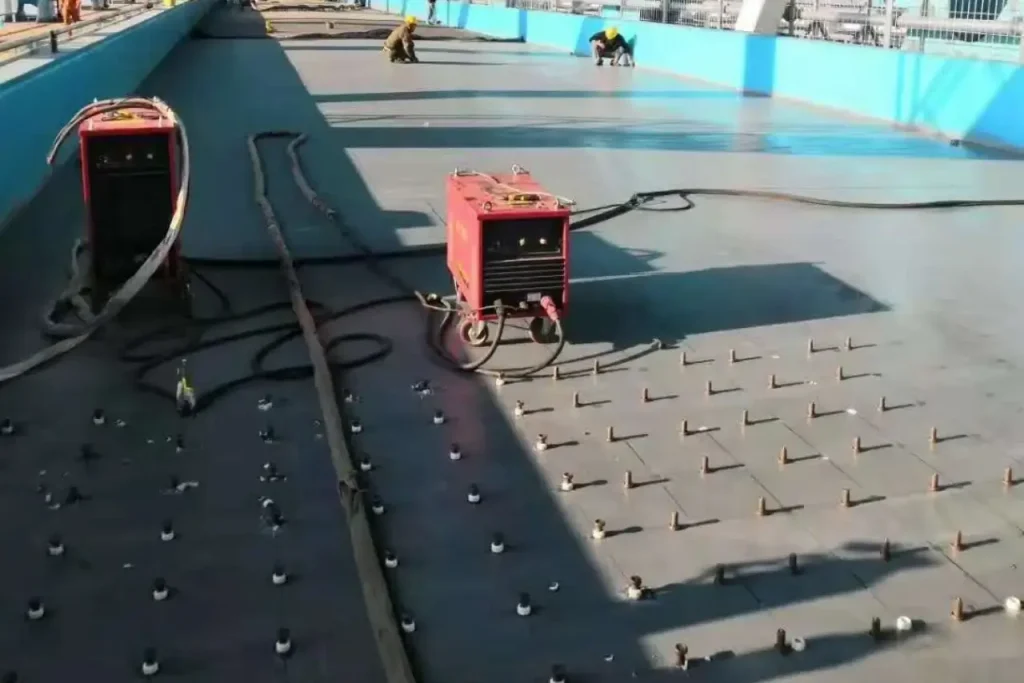
A structural drawn arc stud welder combines a power source, compatible gun, leads, return clamps, studs, and ferrules. Ask the supplier to confirm the complete setup for the largest stud and the actual site conditions.
Drawn Arc Power Sources
For large headed connectors on structural steel, drawn arc welding is commonly specified. Check the project procedure before substituting a short-cycle or capacitor discharge system.
Through-deck welding adds another question: can the selected stud, ferrule, gun, and power source make an approved weld through the actual deck profile and coating?
- Rated current and time range for the specified stud.
- A gun and leads sized for the job.
- A documented duty cycle at the relevant output.
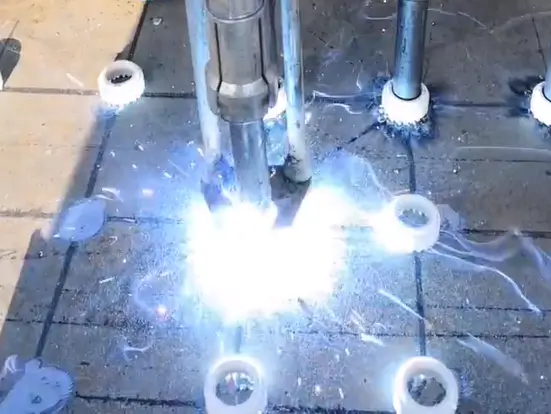
In drawn arc welding, the gun lifts the stud, the arc melts the stud end and base metal, and the gun plunges the stud into the pool. The settings and movement must work together; a machine with adequate current can still produce a bad weld if the gun binds or the return path is poor.
Where Short-Cycle Welding Fits
Short cycle welding can suit certain smaller studs and thinner materials. It is not a blanket substitute for the drawn arc procedure specified for a structural shear connector. Check the approved stud type and process rather than a diameter cutoff in a general article.
If the drawing specifies a headed connector through decking, obtain a procedure and equipment recommendation for that joint. Test welds on representative steel and deck material before production.
Compare machine specifications with the stud maker’s requirements and the project welding procedure.
The table below lists buying checks; current range and duty cycle must come from the specific model datasheet at the relevant output.
| Machine class | Output to verify | Duty-cycle question | Stud-size question | Site power check |
|---|---|---|---|---|
| Drawn arc inverter | Rated current and time range | Rating at required output | Compatible stud and gun | Input phase and capacity |
| Transformer-rectifier | Rated current and time range | Rating at required output | Compatible stud and gun | Input phase and capacity |
A model rated for your stud diameter may still need different leads, a heavier gun, or a different site power supply. Request a complete equipment list.
Check the Drawn Arc Welding Sequence
Set current, weld time, lift, and plunge according to the approved procedure and machine instructions. Make pre-production welds as required, inspect them, and record the settings that pass. The digital display is a way to repeat a setup, not a substitute for testing it.
The Lift, Arc, and Plunge Sequence
Some machines use a pilot arc before the main current. Its purpose and timing depend on the system. Keep the contact area clean even if the controller has a pilot-arc function.
The main arc melts the stud tip and the steel below it. Current and time must be chosen for the stud, steel, deck, cables, and welding position.
- Lift: the gun moves the stud away from the steel.
- Main arc: stud and base surfaces melt.
- Plunge: the gun drives the stud into the weld pool.
When the arc ends, the gun plunges the stud into the molten pool. Check that the stud is centered and the gun moves freely; an uneven collar may indicate a mechanical or return-path problem as well as an electrical one.
What a Ceramic Ferrule Does
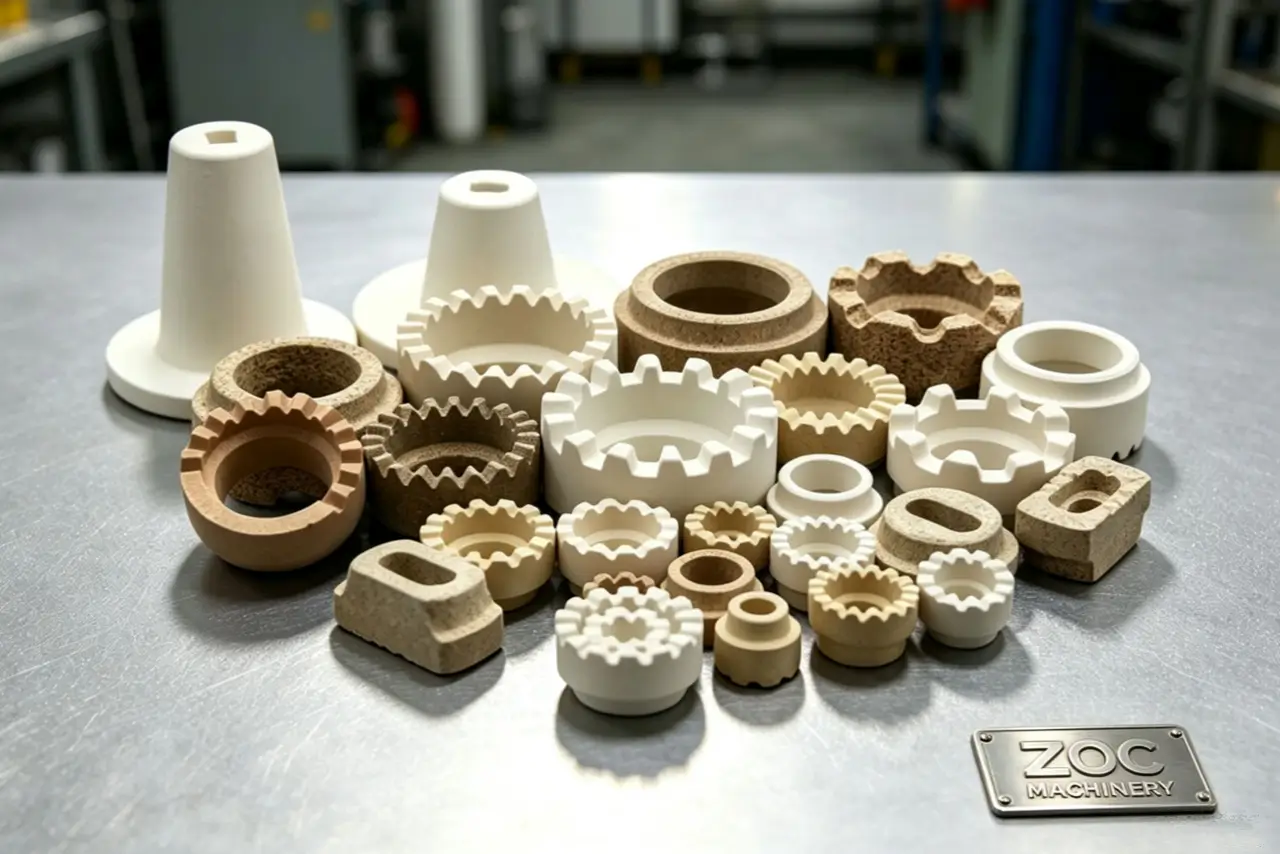
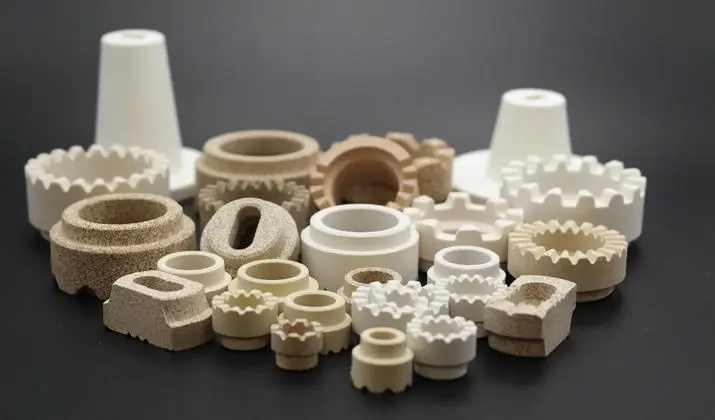
Ceramic ferrules help shield the weld area and shape the collar in many drawn arc procedures. They must fit the stud and welding position. Wet, cracked, or mismatched ferrules can affect the weld.
A ferrule gives useful shielding on an outdoor site, but wind, moisture, contamination, and gun alignment still matter. Follow the procedure for the actual joint.
After changing stud size or position, reset and test the whole cycle. Do not assume a saved program guarantees the same weld.
The phases below are common to drawn arc stud welding. The actual current and timing come from the machine and stud supplier.
| Cycle phase | Timing | Current | Gun action | Operator check |
|---|---|---|---|---|
| Lift and ignition | Per system setting | Pilot arc if equipped | Stud lifts | Clean contact and correct lift |
| Main arc | Per tested procedure | Per stud and machine | Arc melts both surfaces | Stable arc and return path |
| Plunge | Per gun setup | Arc ends per controller | Stud enters weld pool | Free travel and even collar |
A short arc time does not make every stud weld a sub-second operation once loading, positioning, ferrule removal, and inspection are counted.
Example: Planning a 19 mm Through-Deck Job
Suppose a contractor needs to weld 19 mm headed studs through galvanized decking. A candidate inverter drawn arc stud welding machine should be checked against the deck profile, flange thickness, stud and ferrule design, gun reach, site power, and specified inspection. A catalog diameter rating alone is not enough.
Before asking for a quote, collect these five details:
- Specified stud: 19 mm headed connector.
- Actual deck profile, coating, and thickness.
- Beam grade and flange thickness.
- Welding position, cable route, and site power.
- Inspection and production-rate requirements.
Ask the supplier for a setup recommendation, then make trial welds on representative materials under the project procedure. Record the tested settings and any limits on cable length or weld rate.
Which Construction Teams Need These Machines?

Steel fabricators, decking crews, bridge contractors, and industrial installers may all use stud welders, but their equipment needs differ. The stud diameter, welding position, site access, and daily workload are more useful buying inputs than the project label.
Composite Floors in Buildings
On composite floors, the crew may have many studs to weld before concrete is placed. Check how quickly the power source can repeat the required weld without exceeding its rated duty cycle.
Poor access, long leads, an unsuitable gun, or a shortage of ferrules can slow the work even when the power source has spare capacity.
- Rated output for the largest specified stud.
- Duty cycle at the planned weld rate.
- Compatible gun, cables, and return clamps.
Set the inspection plan before mobilization. Project documents may require visual checks, bend tests, or other production controls; a high-output machine does not make those steps optional.
Bridges and Heavy Infrastructure
Bridge work can add difficult access, long cable runs, and more demanding quality records. Select equipment for the specified stud and procedure, then check how it will be moved and powered on site.
If a generator supplies the welder, obtain the machine’s input requirements and test the setup with the intended cable runs. Ask the supplier how voltage variation and lead length affect available welding current.
A suitable system is the one your crew can power, position, maintain, and verify under the project conditions.
Use the project examples below to frame supplier questions, not as universal daily production targets.
| Project type | Volume to confirm | Joint detail | Machine question | Site constraint |
|---|---|---|---|---|
| Composite floor | Stud count and shift plan | Through-deck or direct-to-beam | Rated stud range and duty cycle | Deck and flange access |
| Bridge deck | Stud count and inspection plan | Approved connector and WPS | Output with planned cable run | Power and equipment movement |
| Industrial structure | Stud count and mixed sizes | Attachment and structural details | Gun and preset compatibility | Position and service access |
Crew size, access, deck layout, testing frequency, and machine duty cycle determine the actual rate.
When CD Welding Is the Wrong Process
A Capacitor Discharge (CD) system is useful for many small studs on thin sheet, but it is usually not the process specified for large headed shear connectors on composite beams. Confirm the approved welding process for the structural joint before buying a portable machine.
CD and Drawn Arc Serve Different Jobs
Capacitor discharge machines release stored electrical energy in a very short pulse. That is a different process from the longer controlled arc used for many structural shear connectors.
The shorter pulse suits some smaller attachments and thin base metal. It does not mean every CD weld is weak, or that every drawn arc weld is strong; each has a defined application and inspection method.
- Process approved for the structural connector.
- Stud and base-metal combination within machine limits.
- Representative test welds before production.
A CD unit should not be chosen for a 19 mm composite shear connector because it looks portable or inexpensive. Check whether it is rated and approved for the specified stud and base material.
Current and Time Depend on the Joint
Structural steel and larger weld faces often call for a drawn arc setup that can deliver the current and time specified by the stud and equipment maker. Cable length and return contact affect what reaches the arc.
Welding through galvanized decking requires a qualified combination of stud, ferrule, deck, beam, and machine. Do not assume more current will compensate for a changed deck coating or poor contact.
Choose the process named by the connection detail and confirm it with representative test welds.
The table compares common process uses without turning them into universal size or thickness limits.
| Selection factor | Capacitor discharge (CD) | Drawn arc |
|---|---|---|
| Typical use | Smaller studs and thin sheet | Larger studs and many structural connectors |
| Weld cycle | Short stored-energy discharge | Controlled arc and plunge |
| Base material | Within rated material and thickness | Within approved joint procedure |
| Site conditions | Check coating and power source | Check ferrule, cable, and return |
Ask the supplier to show the tested operating range for your actual stud and deck arrangement.
How to Choose a Stud Welding Machine for Steel Construction
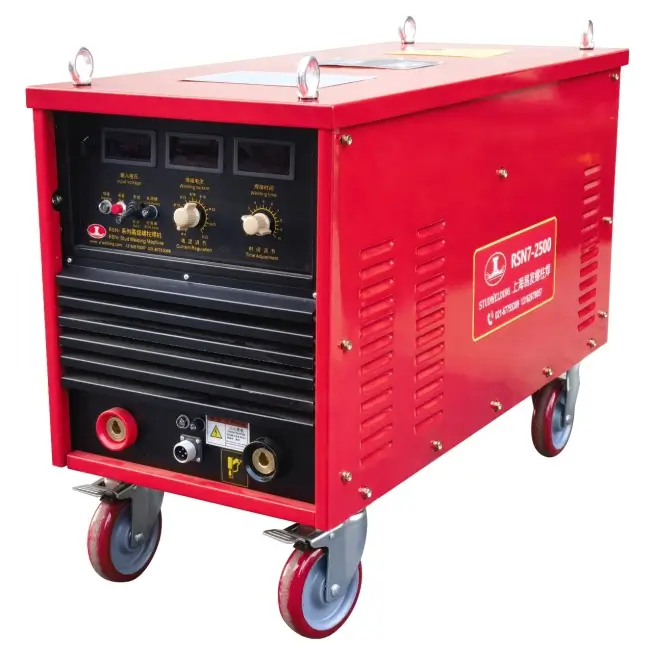
When buying a drawn arc stud welder for structural work, start with the largest stud in the job, then check output at the required weld time, rated duty cycle, gun compatibility, cable run, and site input power. Compare the delivered package, not just the nameplate current.
Start with Stud Size, Output, and Duty Cycle
Duty cycle is tied to a stated output and test condition. Ask how many of your specified welds the machine can make in a shift with the planned cable length and ambient conditions.
If the power source must cool between welds, that delay belongs in the production plan. A larger rating may help, but only if the rest of the system is sized for it.
- Ask for duty cycle at the required output, not only at maximum current.
- Confirm the machine and gun cover the largest weld-base diameter.
- Review cooling, ambient-temperature limits, and maintenance access.
Preset memory can reduce setup errors when a crew changes stud sizes. Record the approved settings and restrict changes to trained operators. Presets cannot identify a wet ferrule or a dirty clamp.
Check Site Power and Cable Runs
Construction sites may run from generators or long temporary feeds. Check the machine’s input voltage, phase, frequency, and rated input capacity against the site supply.
Also check the output cable size and maximum recommended run. Voltage compensation features have limits; a damaged lead or poor return clamp still needs repair.
Ask for the duty-cycle curve, input requirements, gun and cable compatibility, and local service arrangements before comparing prices.
Use this checklist to shortlist models for the specified stud range. Confirm all figures in the current datasheet and with test welds.
| Stud range to assess | Current information needed | Power-source check | Duty-cycle check | Protection check |
|---|---|---|---|---|
| Up to 16 mm | Use stud and machine data | Confirm approved process | At planned weld rate | Input and thermal limits |
| Around 19-22 mm | Confirm through-deck requirement | Check gun and cable fit | At required output | Fault and phase protection |
| Around 25 mm | Request model-specific data | Verify full equipment package | Allow site conditions | Cooling and service plan |
The largest stud on the drawing is a starting point, but the welding position and through-deck detail may set the harder requirement.
Estimate Labor and Downtime Honestly
The best stud welding machine for steel structure construction is not necessarily the one with the highest output. Estimate the cost per acceptable weld: equipment, crew time, consumables, inspection, repairs, power, and downtime. Use your own project quantities rather than a generic payback claim.
Count the Whole Installation Cycle
Track the number of studs placed and accepted per shift during a trial. Include walking, loading, clamp moves, and inspection time; the arc cycle alone is not a production rate.
Compare labor on the same connection and acceptance standard. A manual welding method may not be an approved substitute for a headed connector detail.
- Include positioning and ferrule handling in the schedule.
- Track repairs and rejected welds as part of cost.
- Allow time for the specified inspection and testing.
drawn arc stud welding does not produce stick-welding slag, but a ferrule may need to be removed and the collar inspected. Spatter and rework can still occur when the setup is wrong.
Plan for Service and Spares
A breakdown costs more when the crew and concrete pour are waiting. Ask what parts commonly fail, what can be replaced on site, and who can support the machine during the job.
Keep spare chucks, ferrule grips, leads, clamps, and other consumables suited to the machine and stud sizes. Compare lead times for control boards or gun repairs before mobilization.
A purchase pays off when the equipment produces acceptable welds at the rate the project needs. Measure that on the job rather than promising a fixed return.
The table turns a cost claim into figures you can collect during a trial or from your own site records.
| Cost item | Current method | Candidate stud welder | Evidence to collect |
|---|---|---|---|
| Installation time | Measure the existing cycle | Measure accepted studs per shift | Same joint and access |
| Repairs and rework | Record rejects and repair hours | Record trial and production results | Apply same inspection criteria |
| Consumables and cleanup | List process-specific materials | Include ferrules and removal | Price the full installed joint |
Once you have trial-weld data, compare the full installed cost with the alternatives allowed by the design.
Safety, Inspection, and Compliance
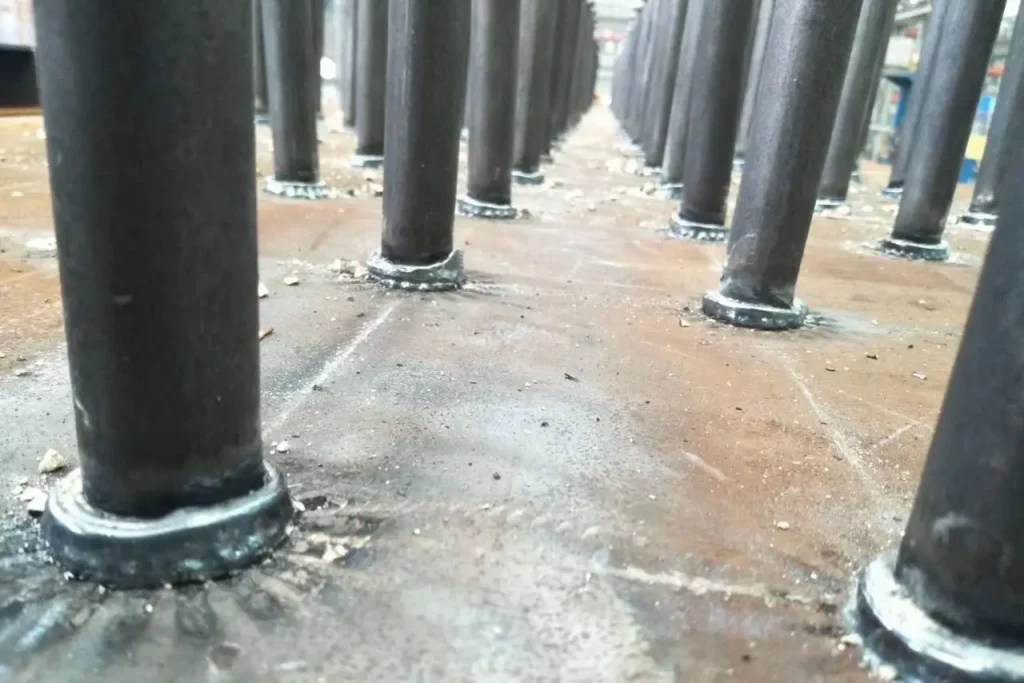
A structural stud welder is an electrical welding machine, not an inherently safe one. Specify the correct input protection, grounding, thermal limits, and gun setup. Operators still need the site’s welding controls and protective equipment.
Electrical and Thermal Protection
Ask which protective functions the quoted model actually has and how a fault is shown to the operator.
Thermal shutdown, phase-loss detection, and over-current protection vary by machine. Review the manual rather than assuming that every digital controller includes them.
- Input protection and suitable site electrical supply.
- Thermal protection and a clear fault indication.
- Correct return and cable connections.
Choose stud welding guns with a compatible chuck and ferrule grip, enough reach for the deck profile, and a weight operators can manage in the required position.
Test the Weld, Not Just the Machine
Stable current helps repeatability, but weld quality also depends on the stud, steel, surface, ferrule, return path, lift, and plunge. Inspect and test the weld under the applicable procedure.
A weld that looks even can still be unacceptable. The project specification sets the inspection and testing requirements for structural connectors.
Use the required pre-production and production checks. Never treat a machine certificate as a substitute for an accepted stud weld.
Separate machine protection features from welding-code tests when reviewing a quotation.
| Check | Evidence to request | Why it matters | Field confirmation |
|---|---|---|---|
| Thermal protection | Machine manual and rating | Limits overheating | Verify fault indication |
| Electrical protection | Input and protection specifications | Matches site supply | Inspect connections and grounding |
| Weld acceptance | Approved procedure and code edition | Tests the actual joint | Record required inspections |
Confirm the applicable standard edition and project acceptance criteria with the engineer or inspector.
Digital Controls and Inverter Power Sources
Digital controls can make current and time easier to set and repeat. Some models also store programs or display fault codes. These features are useful, but they do not automatically correct every change in site voltage or operator technique.
Parameter Memory and Fault Codes
Transformer-rectifier machines and inverter machines can both be suitable when rated for the job. Compare their actual output, controls, weight, serviceability, and site power requirements.
Changing stud diameter still calls for the right ferrule, chuck, gun settings, and trial weld. A saved program reduces re-entry; it does not remove setup work.
- Programs for approved stud sizes and settings.
- Fault information that operators can understand.
- Current and time adjustment within the required range.
Fault indications can shorten troubleshooting if the operator understands them. Ask for the manual and a demonstration of phase, thermal, and cable-related warnings.
Inverter or Transformer-Rectifier?
An inverter may draw less idle power or be easier to move, but the difference depends on the models and workload. Request comparable rated-input and efficiency data before estimating generator size or energy cost.
Weight matters when a machine must be moved across a large site. Check the full transport package, including cables, gun, cart, and power connection.
Select controls your crew can use and your service team can repair. Repeatable settings still need a verified welding procedure.
Use the table as a comparison template, then fill it with data from the two actual models under consideration.
| Feature | Transformer-rectifier model | Inverter model |
|---|---|---|
| Controls | Check actual settings and display | Check actual settings and display |
| Program memory | Verify on quoted model | Verify on quoted model |
| Weight and movement | Compare delivered package | Compare delivered package |
| Input and efficiency | Request rated data | Request rated data |
Technology type alone does not decide weld quality, energy use, or total cost.
Compare Suppliers and After-Sales Support
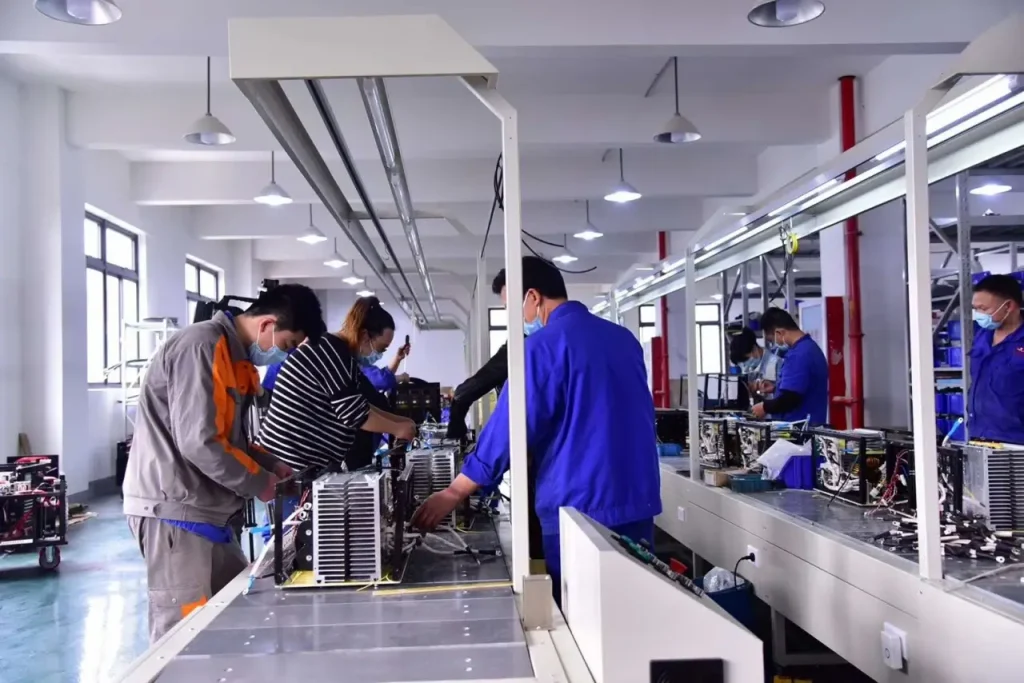
A supplier should be able to document the machine’s rated range, compatible gun and leads, input requirements, parts availability, and support route. Ask the same questions of a factory and a distributor.
Verify What the Supplier Can Deliver
Buying direct can simplify some technical discussions, but only if the manufacturer can support your site and deliver the complete system. Request written specifications and a clear warranty path.
A distributor may offer local stock or faster service. Compare the actual package and support response instead of assuming one channel always costs less.
- Written price for the complete machine, gun, and leads.
- Confirmed delivery and spare-parts lead times.
- Warranty, manuals, and support contact for the jobsite.
Check what a claimed certification covers. ISO 9001 concerns a management system; a CE mark addresses applicable product requirements in its market. Neither by itself proves that a particular stud weld will pass the project inspection.
Ask About Service Before You Buy
Ask for the stock status and lead time of consumables and repair parts. A promised “48-hour” delivery is useful only if it applies to your location and the exact part.
Before purchase, identify who diagnoses faults, how remote support works, and where the machine can be repaired. A spare gun or lead may be worth more than a feature you will never use.
Compare suppliers on documented capacity, compatible accessories, delivery terms, warranty, and service for your jobsite.
Use the table to record what each seller actually commits to in writing.
| Sourcing check | Factory quotation | Distributor quotation |
|---|---|---|
| Price | Include gun, leads, and consumables | Include gun, leads, and consumables |
| Technical support | Name contact and response route | Name contact and response route |
| Spare parts | Confirm stock and delivery time | Confirm stock and delivery time |
| Configuration | Confirm voltage and gun fit | Confirm voltage and gun fit |
Choose the supplier who can support the tested welding setup through the project, regardless of whether the invoice comes from a factory or distributor.
Frequently Asked Questions
Can I weld shear studs through galvanized decking?
Often, yes, when the deck profile, coating, stud, ferrule, machine, and procedure are qualified for through-deck welding. Do not use a single minimum current or deck thickness from a general guide; make representative test welds.
What machine should I use for large-diameter shear studs?
Start with a drawn arc model rated for the specified stud and weld position. Confirm the current and time range, gun, cable length, duty cycle, and site power against the supplier’s data and project procedure.
How can I tell whether the welder is overheating?
Check the temperature or fault indication described in the machine manual and watch for automatic shutdown or a falling permitted weld rate. Stop and investigate ventilation, duty cycle, and electrical connections if it occurs.
Can a three-phase stud welder run from a site generator?
Yes, if the generator can supply the machine’s starting and welding demand at the required voltage, phase, and frequency. Size it from the equipment data and test it with the planned leads and other site loads.
What does a ceramic ferrule do?
It helps shield the molten weld area and shape the collar during many drawn arc stud welds. Use the ferrule specified for the stud, gun, and welding position, then remove it and inspect the weld as required.
Choose the Setup, Then the Supplier
The Final Buying Checklist
Choose the process and complete equipment package from the specified joint. Get written answers on stud range, duty cycle, input power, gun and lead compatibility, through-deck capability, testing, and service. A trial weld on representative material is a better buying check than an unsupported savings claim.
Send the Joint Details with Your Inquiry
Send us the stud drawing or weld-base diameter, steel and deck details, welding position, site power, and expected work volume. contact us for a machine-and-gun recommendation and a quotation you can compare against the project requirements.